Improved Pipeline Productivity

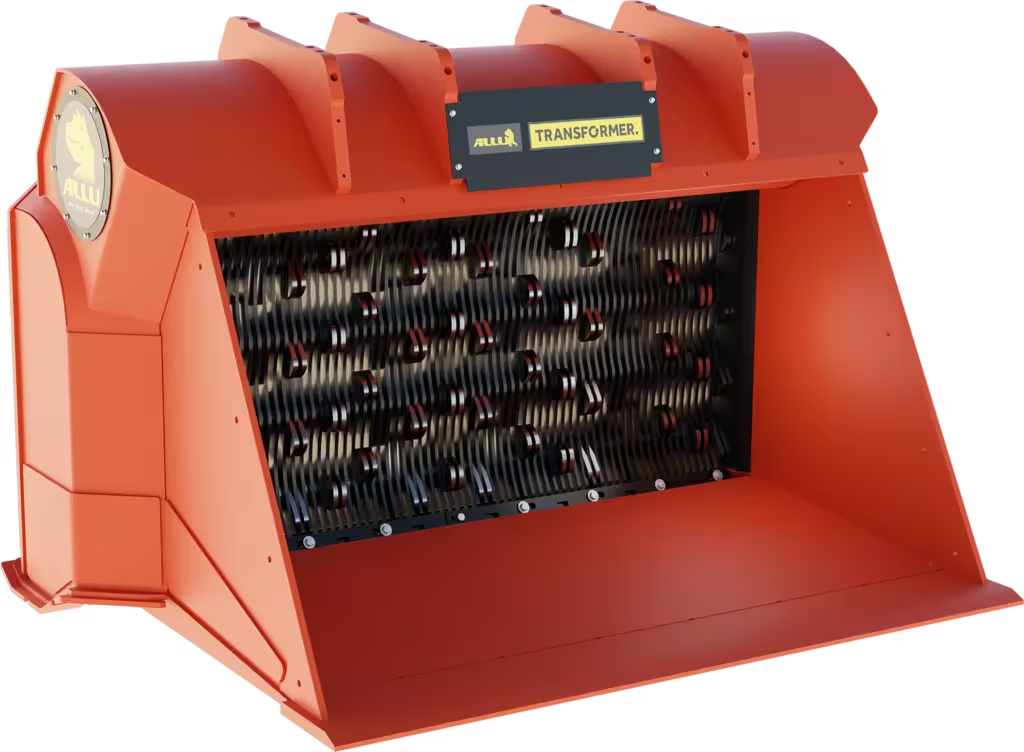
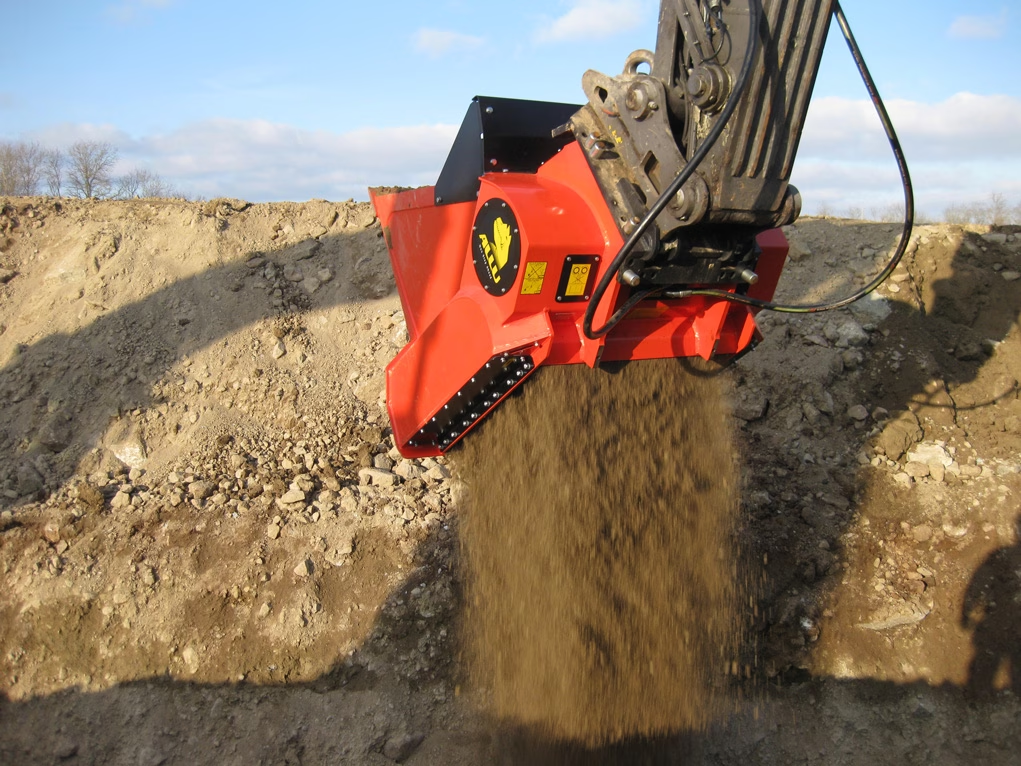
On a five-mile natural gas pipeline project in West Virginia, Momentum Pipeline used an ALLU DH 4-17 Screening Bucket, supplied by Leslie Equipment Company, to turn excavated soil into protective pipeline padding while streamlining material processing on site.
Case study

Improving Pipeline Padding Productivity With Screening Buckets

West Virginia, USA

Material 1 ½” minus material from screened soil

Industry Pipeline Padding

Application Pipeline & utility backfill

Function Padding screened material to backfill and protect pipeline project

Model ALLU DH 4-17 with 25mm XHD blades

On a five-mile natural gas pipeline project in West Virginia, Momentum Pipeline relied on ALLU dealer Leslie Equipment Company and an ALLU Screening Bucket to efficiently process native soil into pipeline padding material directly along the right-of-way. 

Working with Leslie Equipment Sales Representative Pete Culicerto, Momentum Pipeline utilized an ALLU DH 4-17 Screening Bucket with 25 XHD blades mounted on a John Deere 300G excavator. The bucket screened out larger rocks from the excavated soil, producing approximately 1 1/2-inch minus (less than 40 mm) material that could be used to pad and protect the 24-inch steel natural gas pipeline. 

For Momentum Pipeline, the solution built on a relationship with ALLU equipment that has lasted approximately 12 years and has helped transform the company’s approach to pipeline padding. 

Protecting a Five-Mile Natural Gas Pipeline
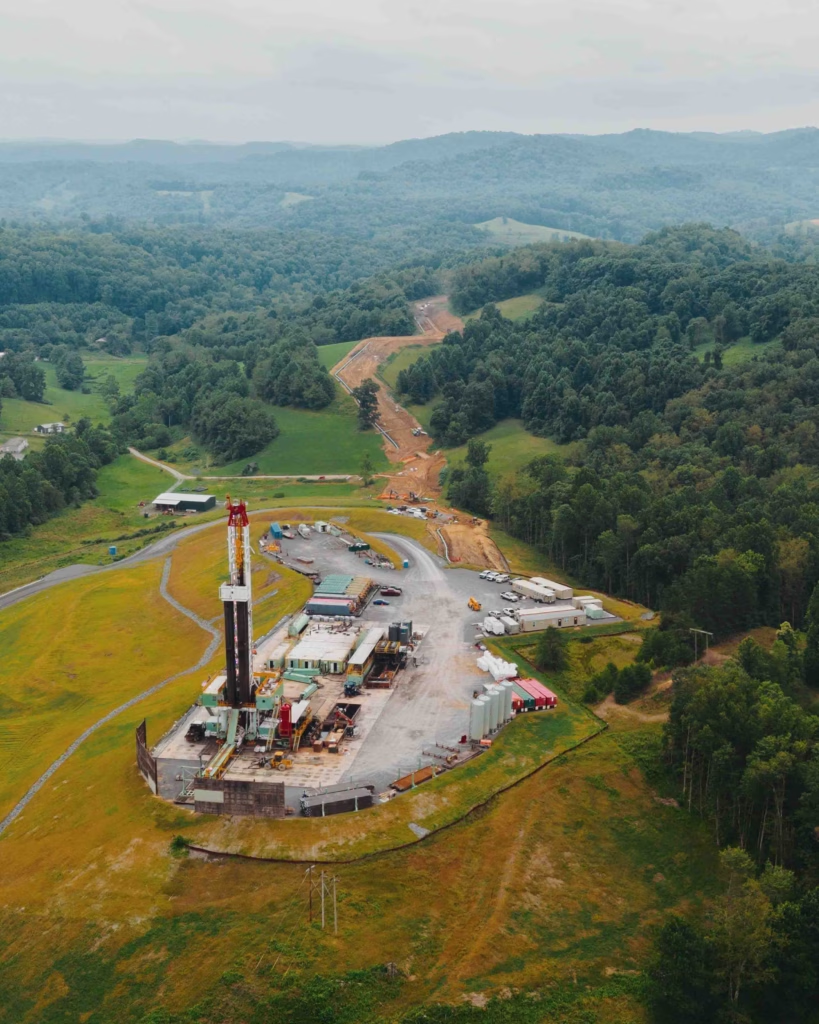
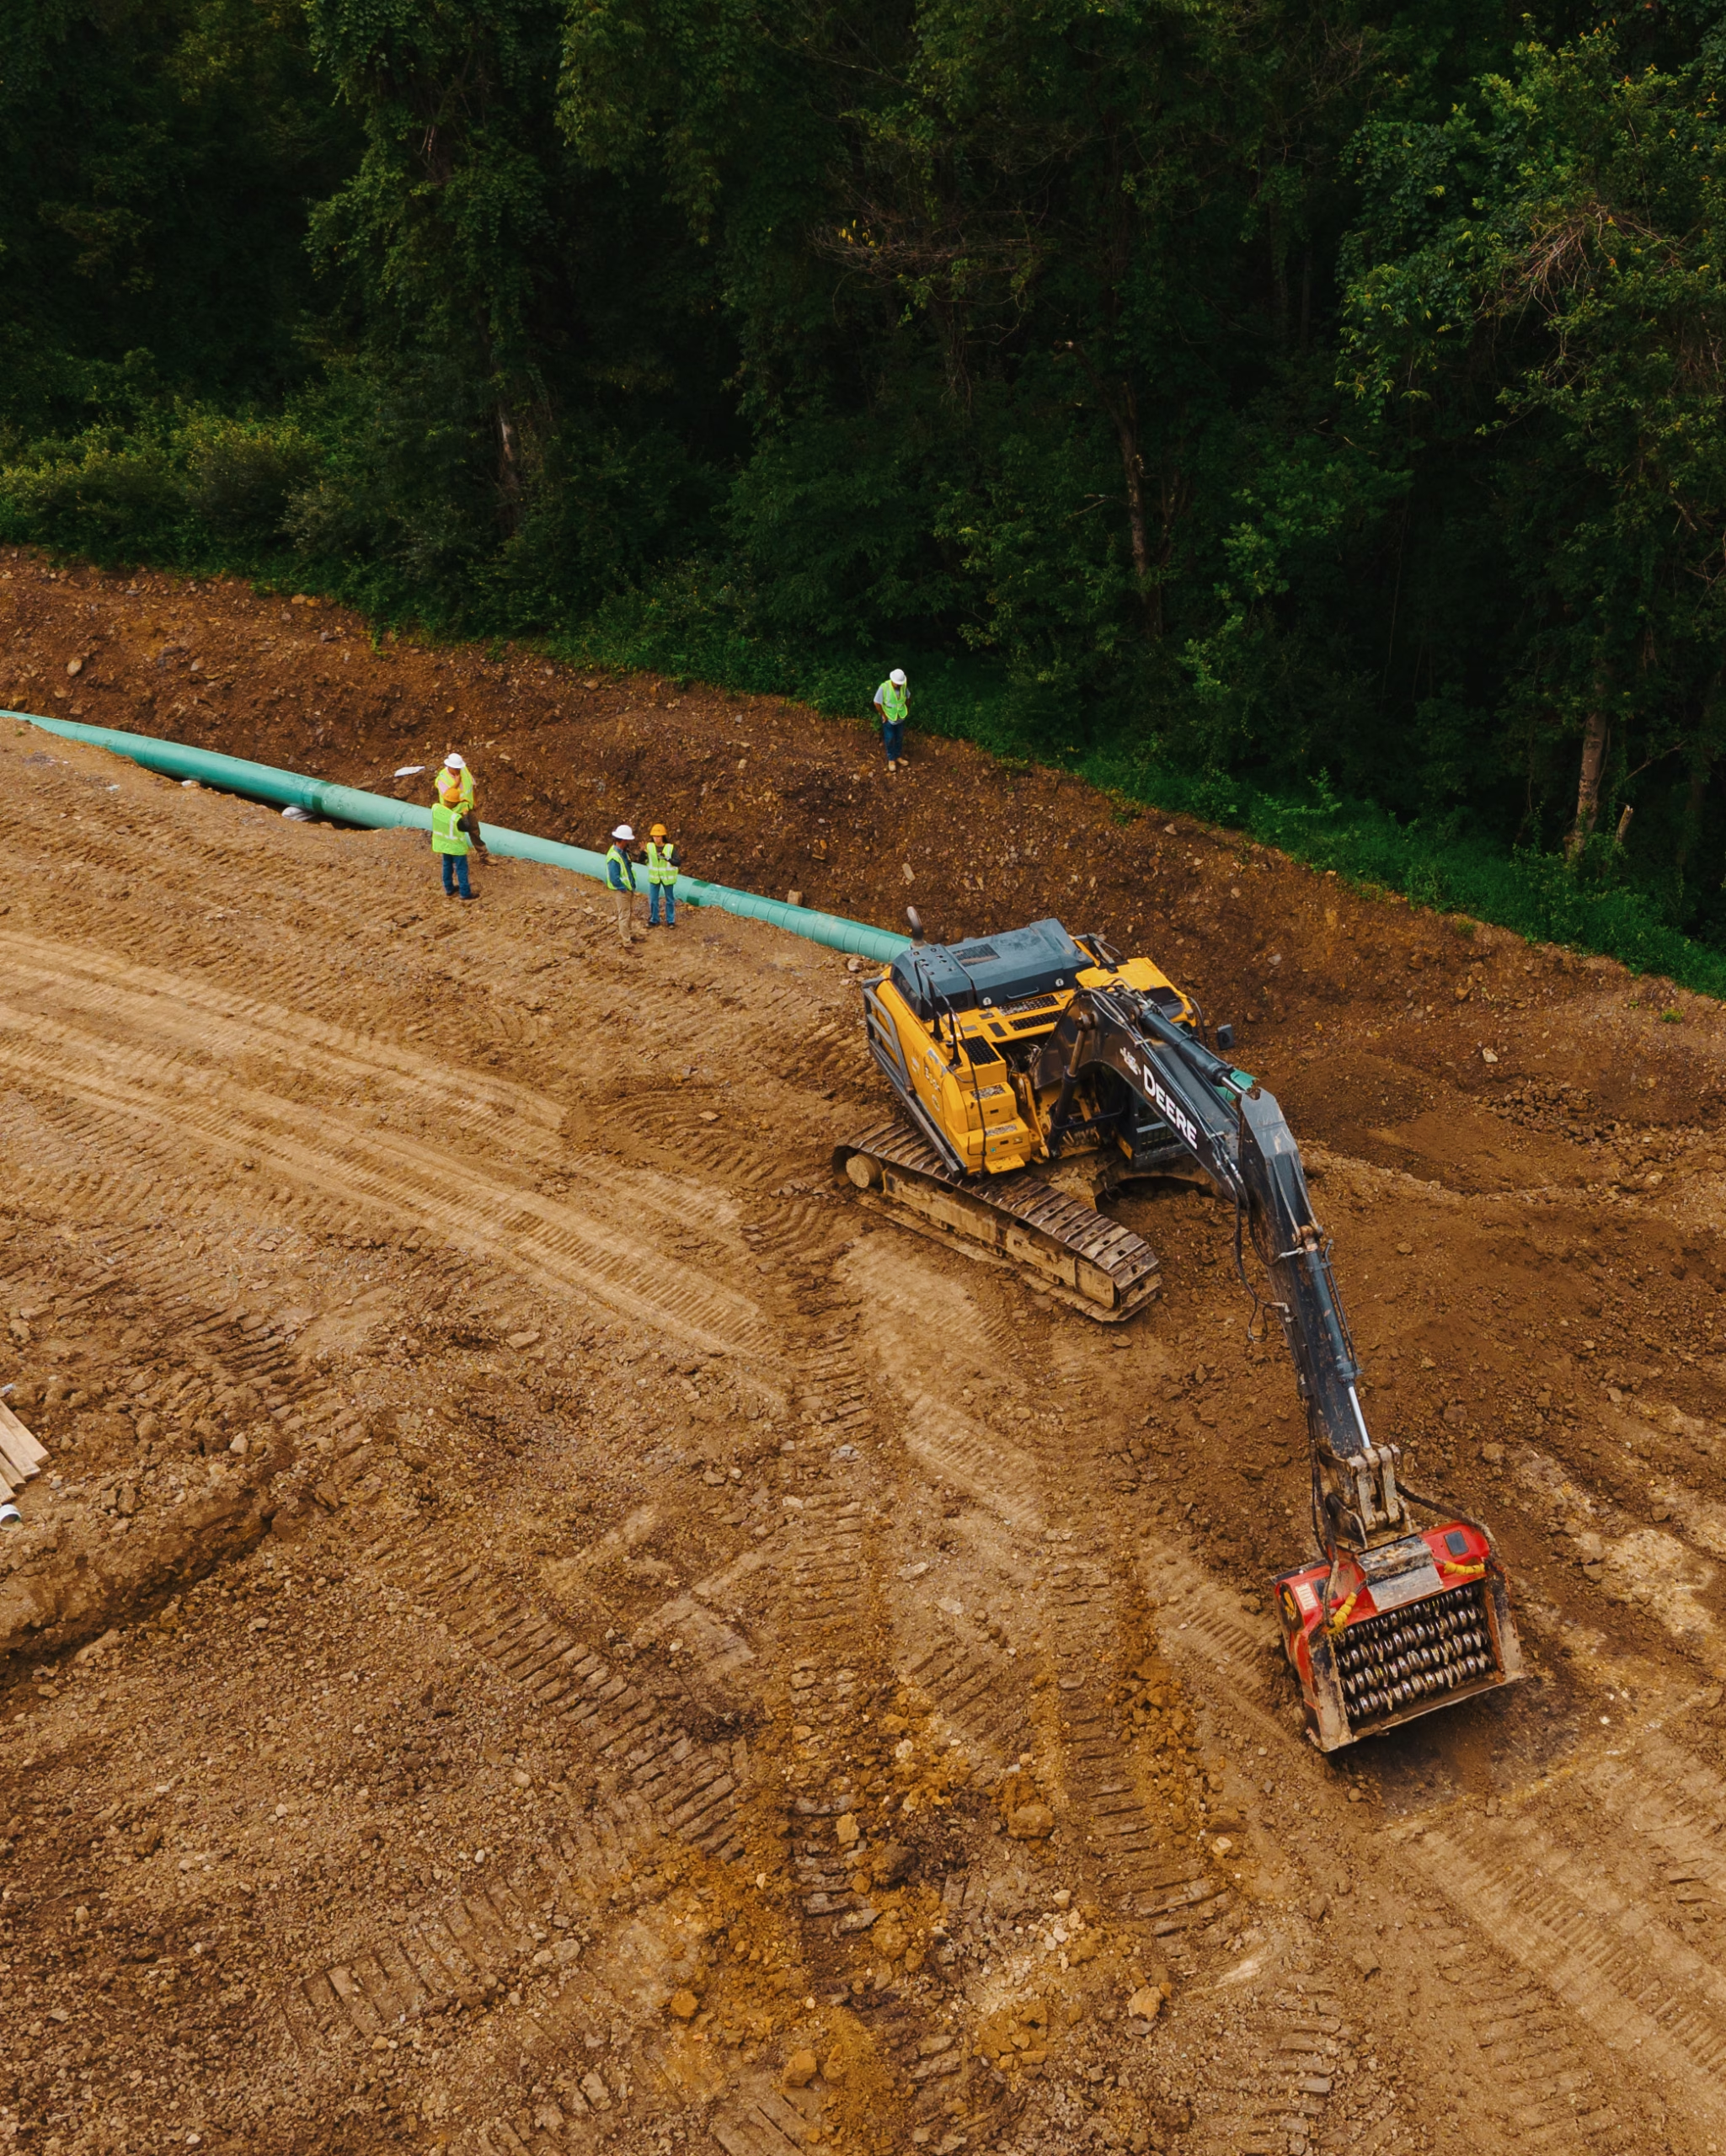
Overhead view of the 5-mile long West Virginia pipeline site with the natural gas drill.
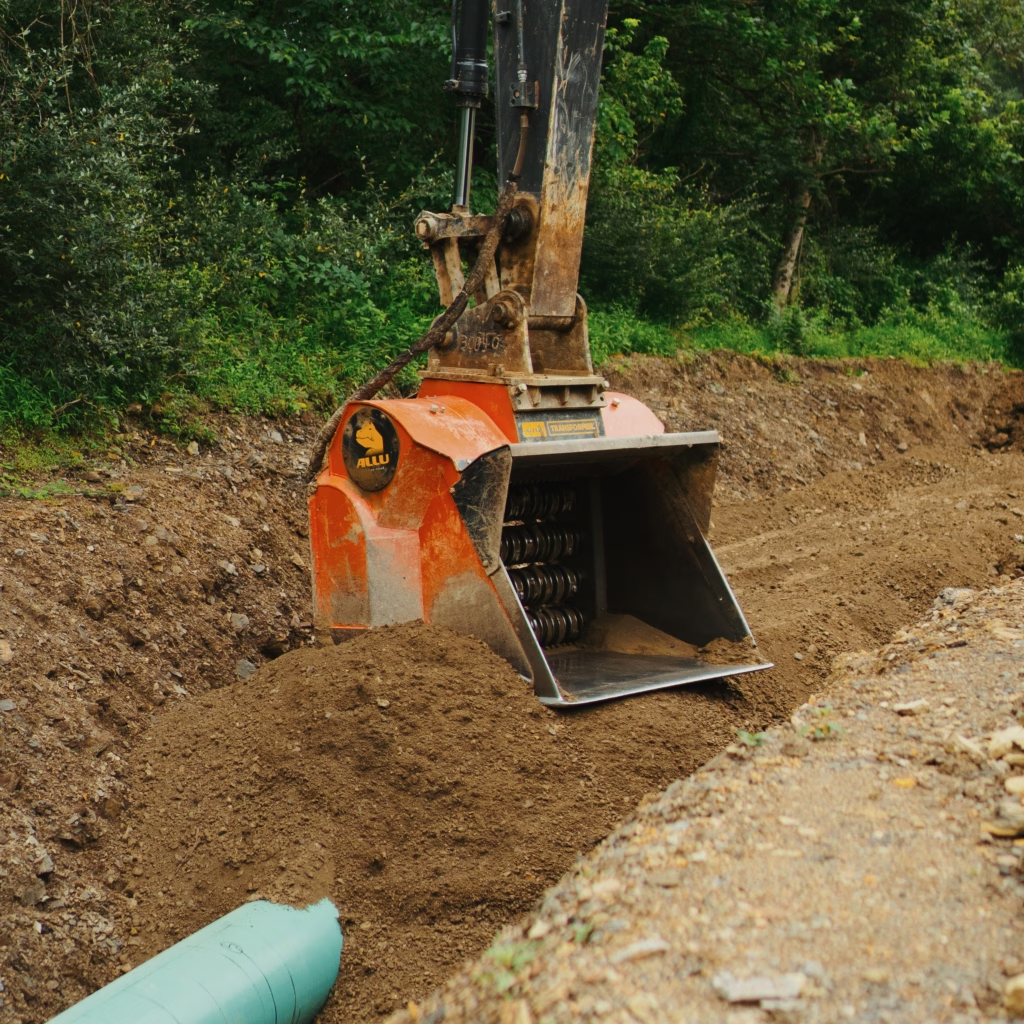
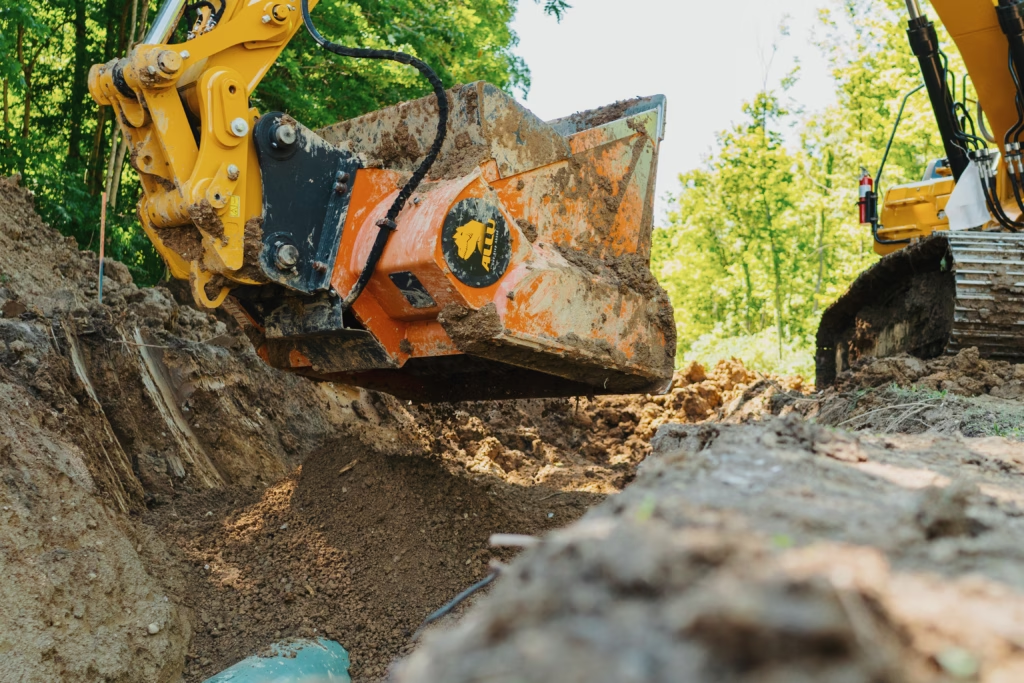
Overview of an excavator and ALLU screening bucket on a pipeline jobsite.

Momentum Pipeline, a West Virginia contractor with more than 20 years of experience, began the project in April 2026. Approximately 75 workers were involved in constructing the five-mile natural gas pipeline, which connected a well pad to a mainline for distribution. 

Proper padding is an important part of pipeline construction. Larger rocks within excavated material can potentially damage the external coating of the pipe during backfilling. Creating a screened layer around the pipeline helps provide protection by removing oversized material before the soil is placed around the pipe. 

For Momentum Pipeline, the goal was straightforward: efficiently screen larger rocks from the excavated material and reuse the processed soil for padding and backfill. 

ALLU and Leslie Equipment Step In

Momentum Pipeline turned to ALLU dealer Leslie Equipment Company for the equipment and support needed for the application. Leslie Equipment has worked with ALLU for years, supplying screening and crushing buckets for pipeline projects and maintaining a fleet of buckets and replacement parts for its customers. 

For sales representative Pete Culicerto, finding the right padding bucket starts with understanding the project. Pipe diameter, excavator size, job size and the required completion schedule can all influence which ALLU bucket and how many units a contractor may need. 

Customers typically use between one and four buckets depending on the scale and timeframe of the project. Leslie Equipment’s inventory allows its team to help match contractors with an ALLU configuration suited to their particular operation. 

“ALLU is the preferred vendor that we use because of the productivity and support, which I tell our customers about,” Culicerto said. 

On the West Virginia project, that solution was an ALLU DH 4-17 Screening Bucket equipped mounted on a John Deere 300G excavator. 

Protecting the Pipeline from the Ground Up

On this project, the 24-inch steel pipeline carries natural gas from the well pad to a mainline, where the gas can continue on for distribution. Once the pipe is installed in the trench, the material placed around it becomes an important part of protecting the pipeline. 
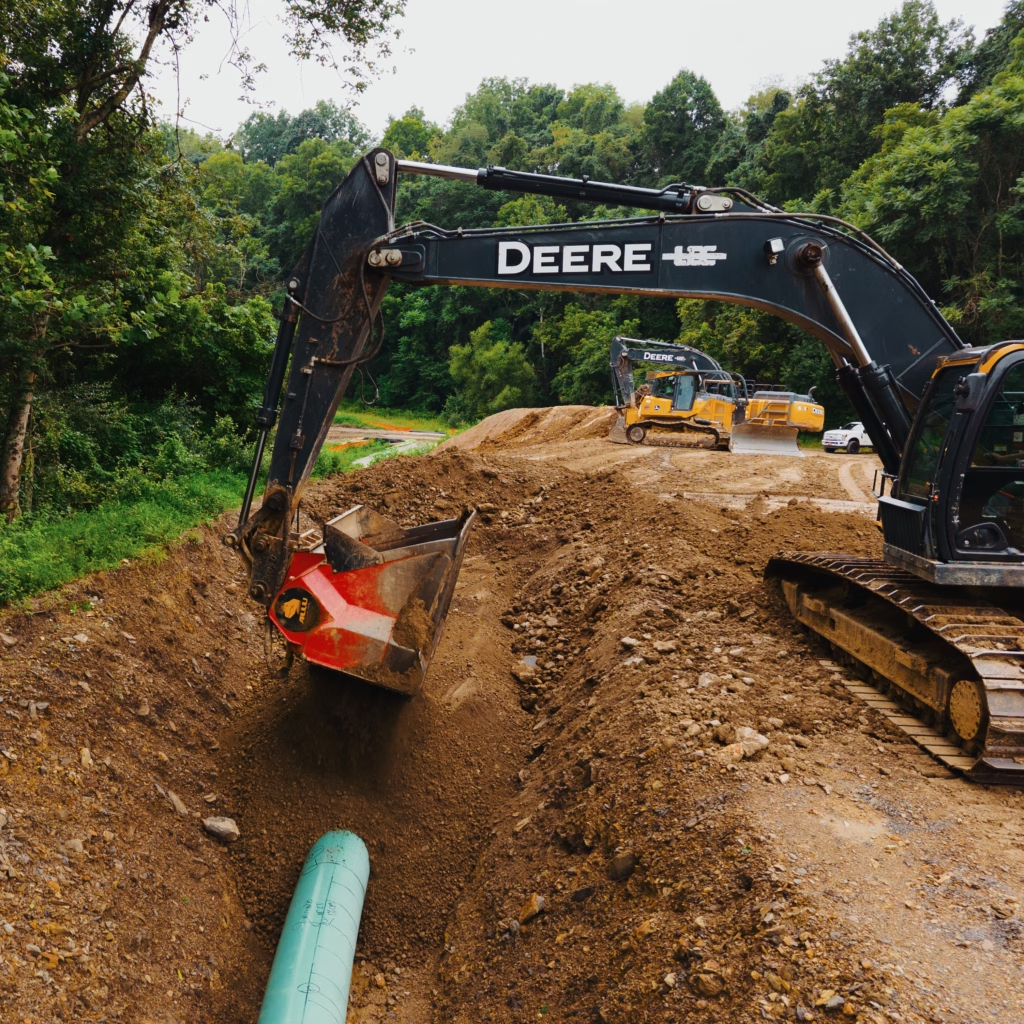
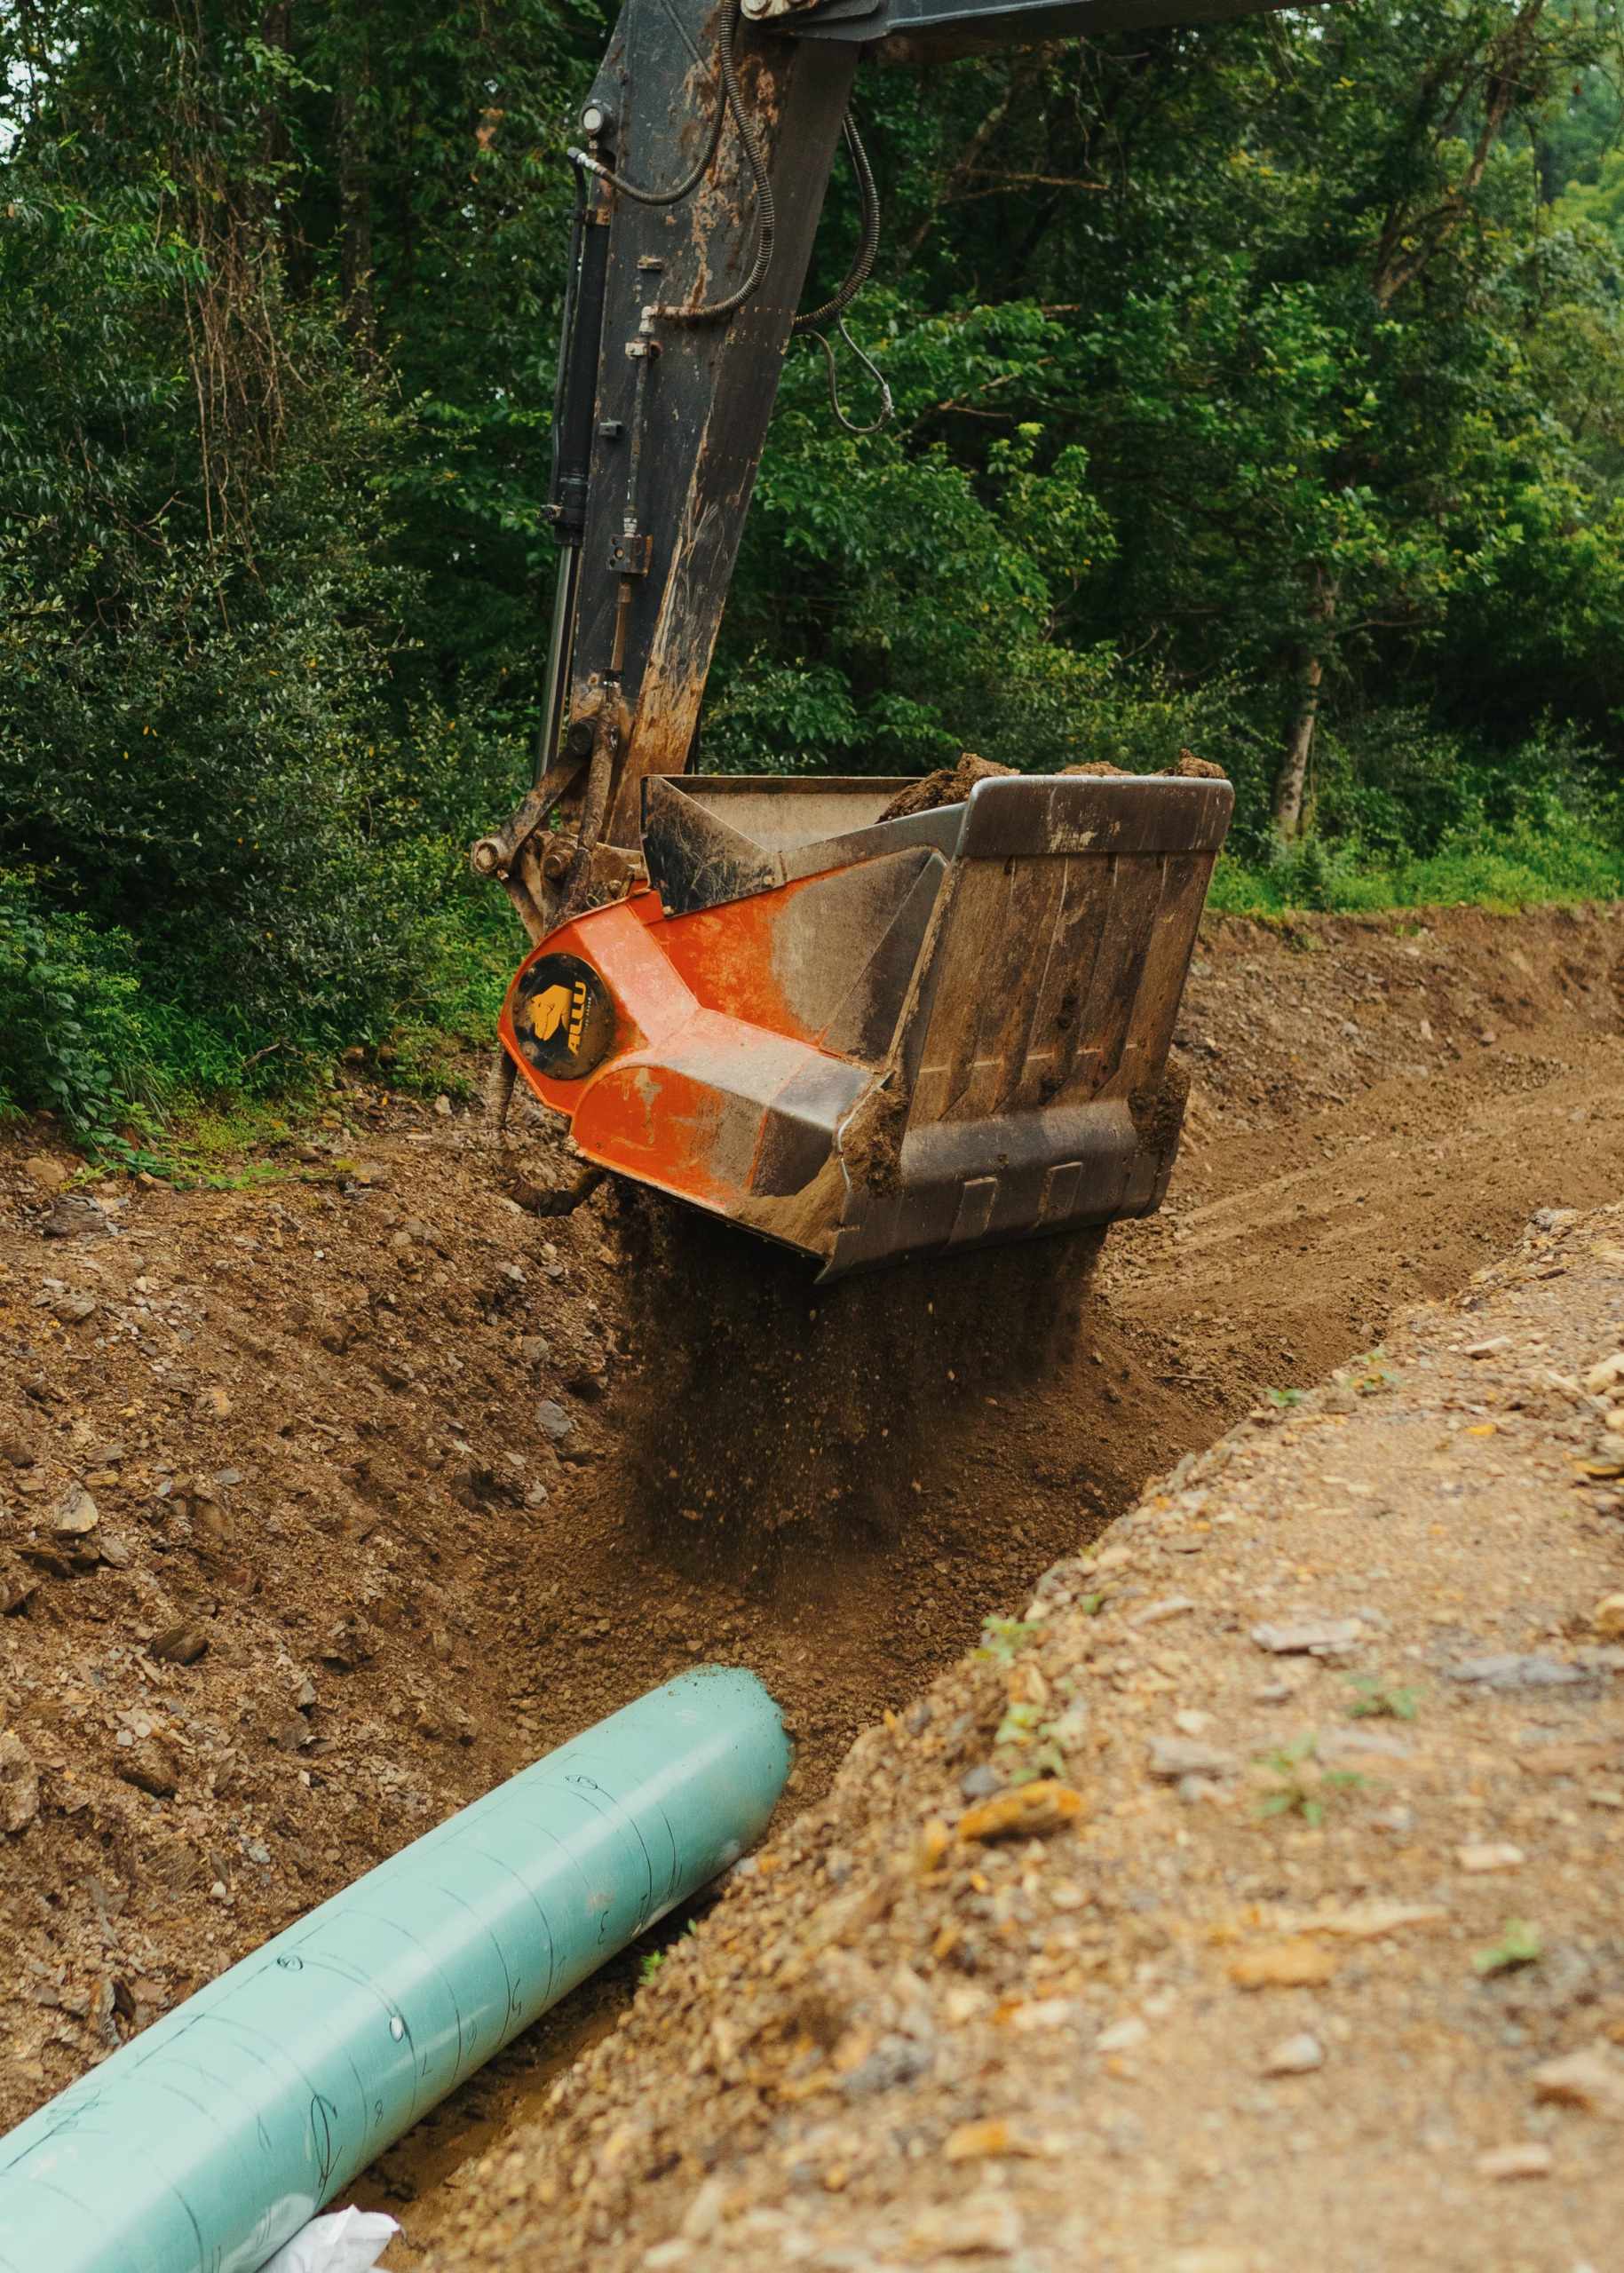
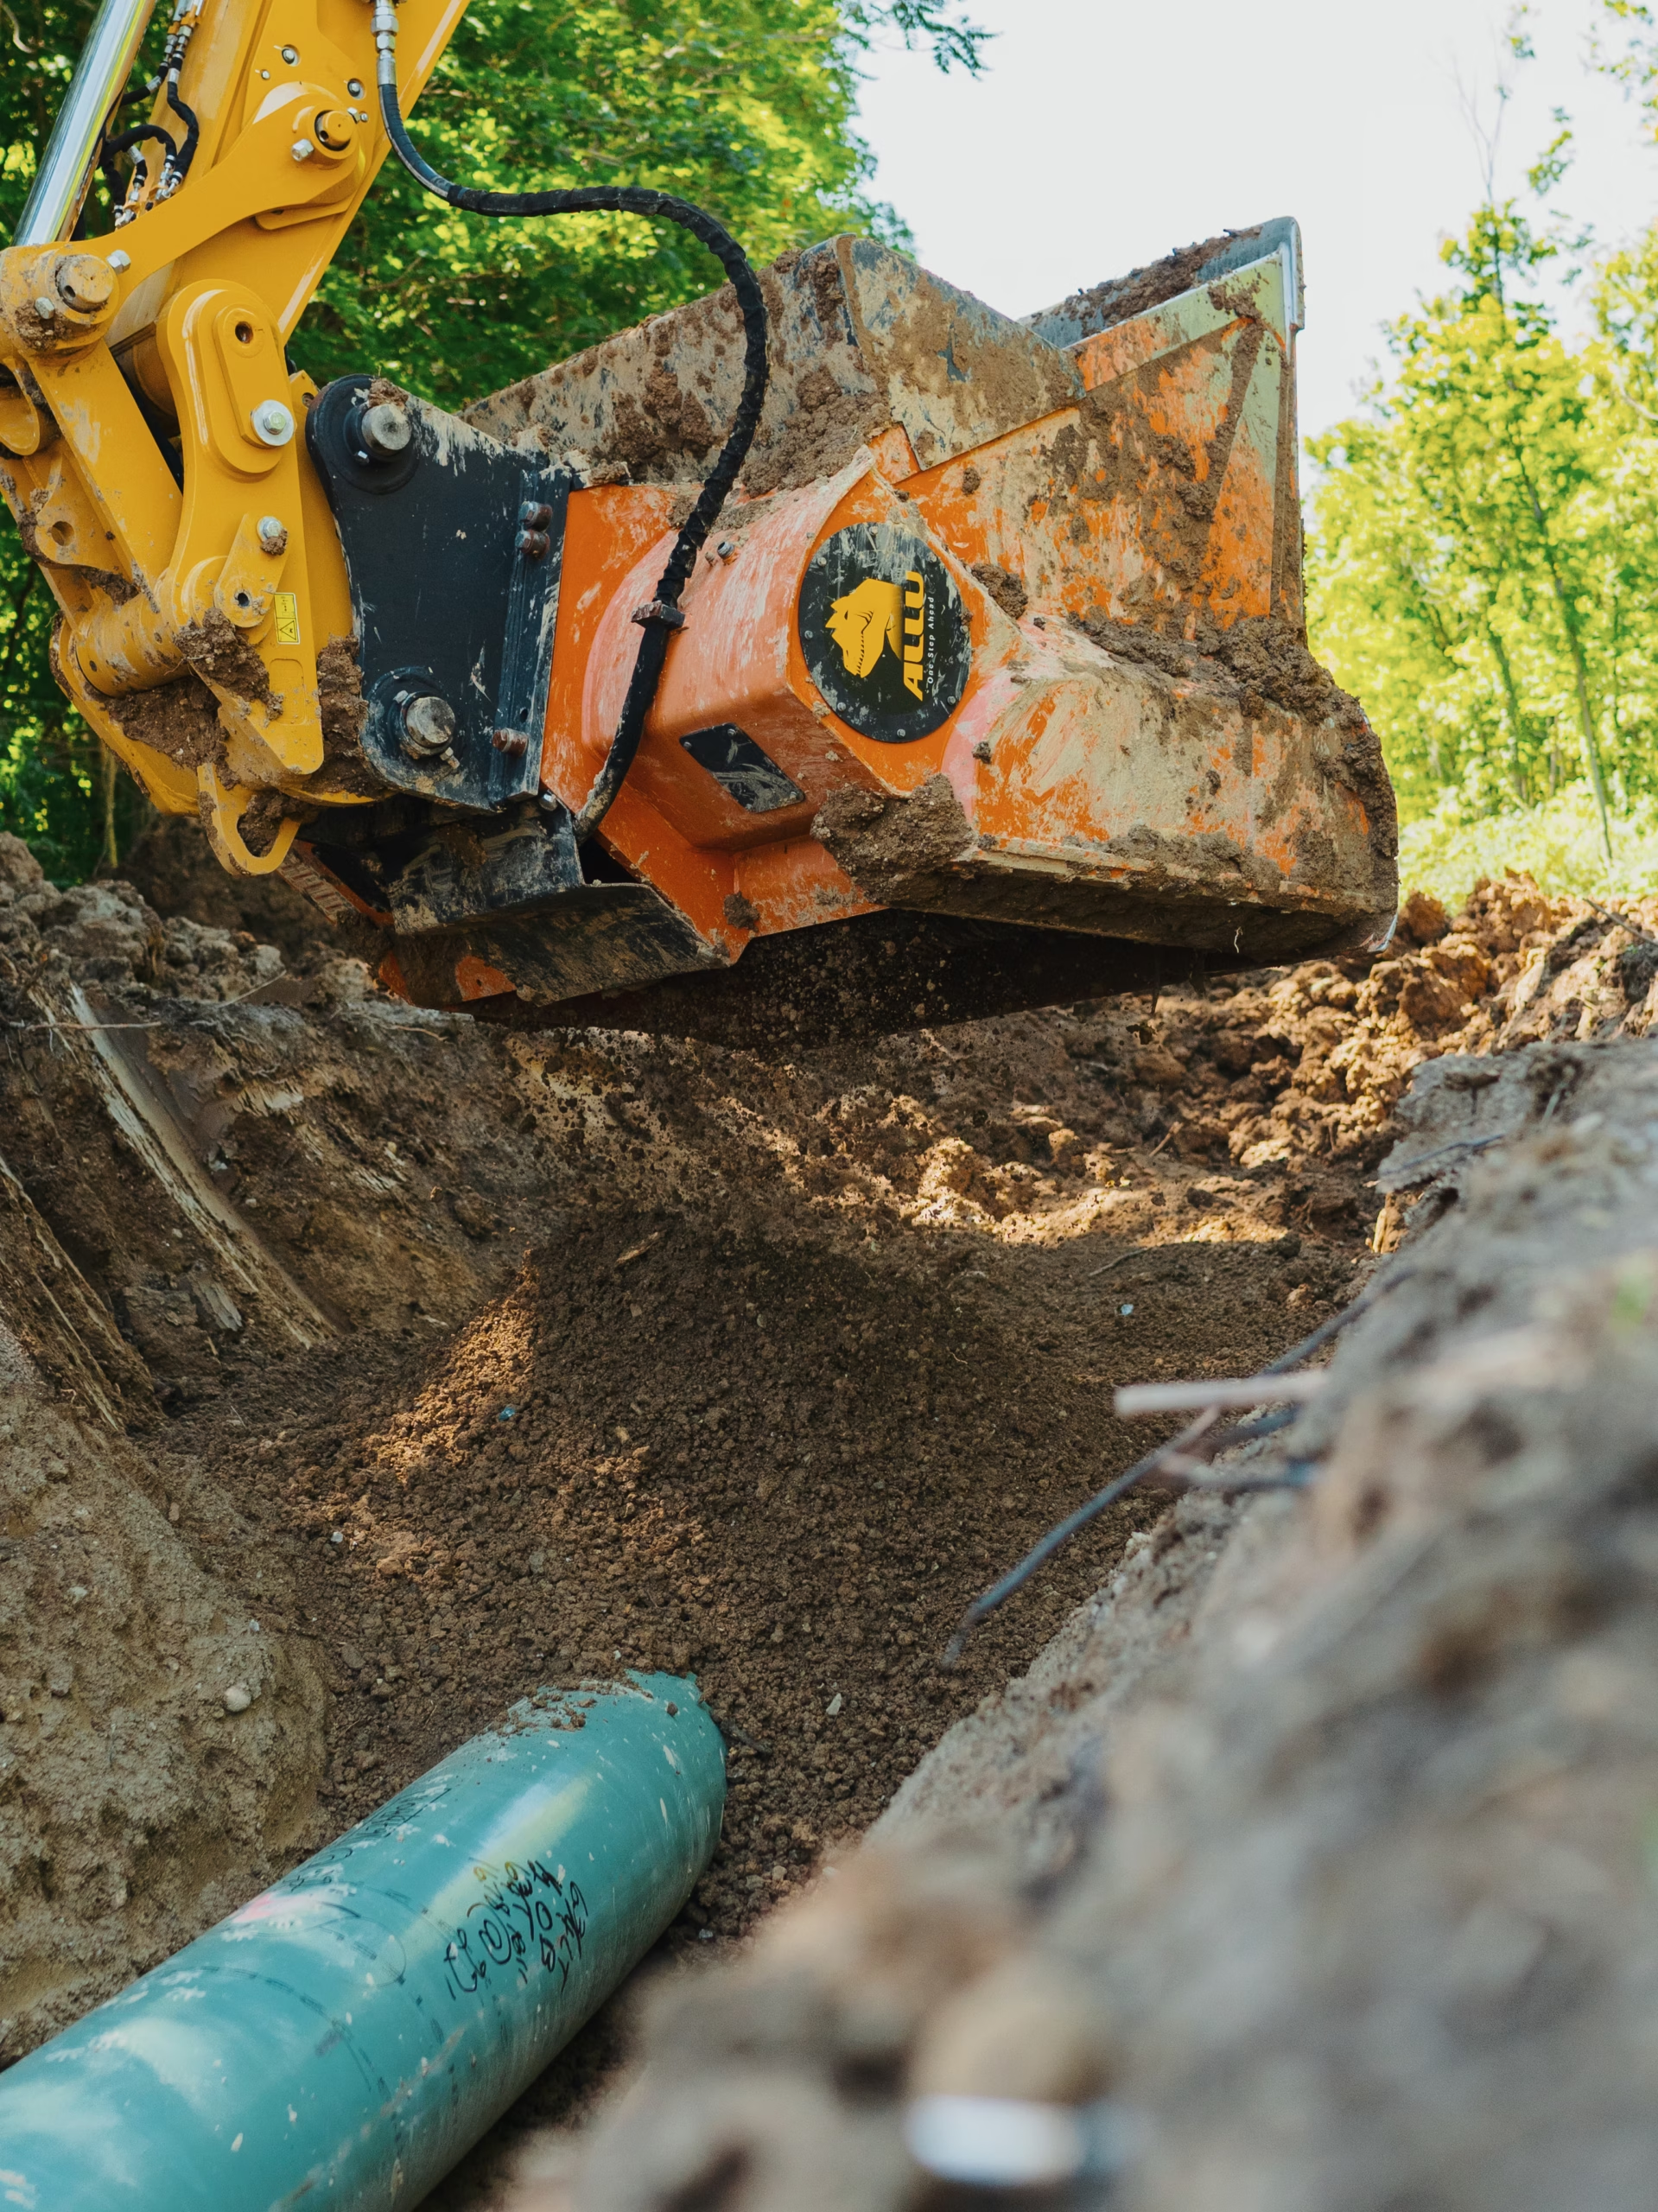
The ALLU screening bucket padding a pipeline ditch with machinery in the background.
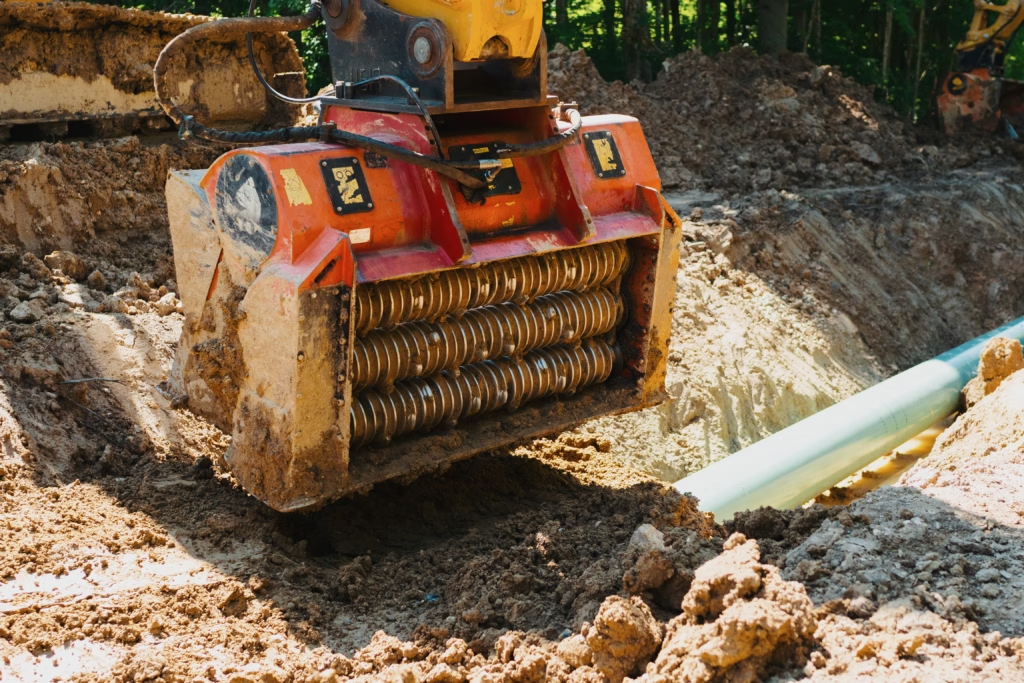
ALLU Screening Bucket on a Pipeline project compacting padding.

Excavated soil can contain larger rocks that could come into contact with and potentially damage the pipe’s protective coating during backfilling. Momentum Pipeline uses the ALLU screening bucket to screen out those larger rocks and produce approximately 40 mm (1 1/2-inch minus) material for padding around the pipe. By processing the native material before it is placed back into the trench, the crew can create a finer layer around the pipeline while reusing material already available on the project. 

Processing Padding Material Where It Is Needed

The ALLU DH 4-17 allowed Momentum Pipeline to screen excavated soil directly along the pipeline and produce smaller than 40 mm material for padding. 

As the ALLU bucket processed the material, an excavator and dozer worked behind the operation to pull up fresh soil and help keep the process moving. Instead of relying on workers to manually identify and remove larger rocks during placement, the bucket screened oversized material before the processed soil was placed around the pipe. 

Production can vary depending on factors such as soil and moisture conditions. According to Culicerto, when material is relatively dry, contractors can typically pad a couple hundred feet of pipeline per day. 

“A lot of this pipe has to be padded back, so an ALLU Bucket is used on every project,” Culicerto said. “If not one, then multiple buckets at the same time.” 

Taking Labor Out of the Ditch
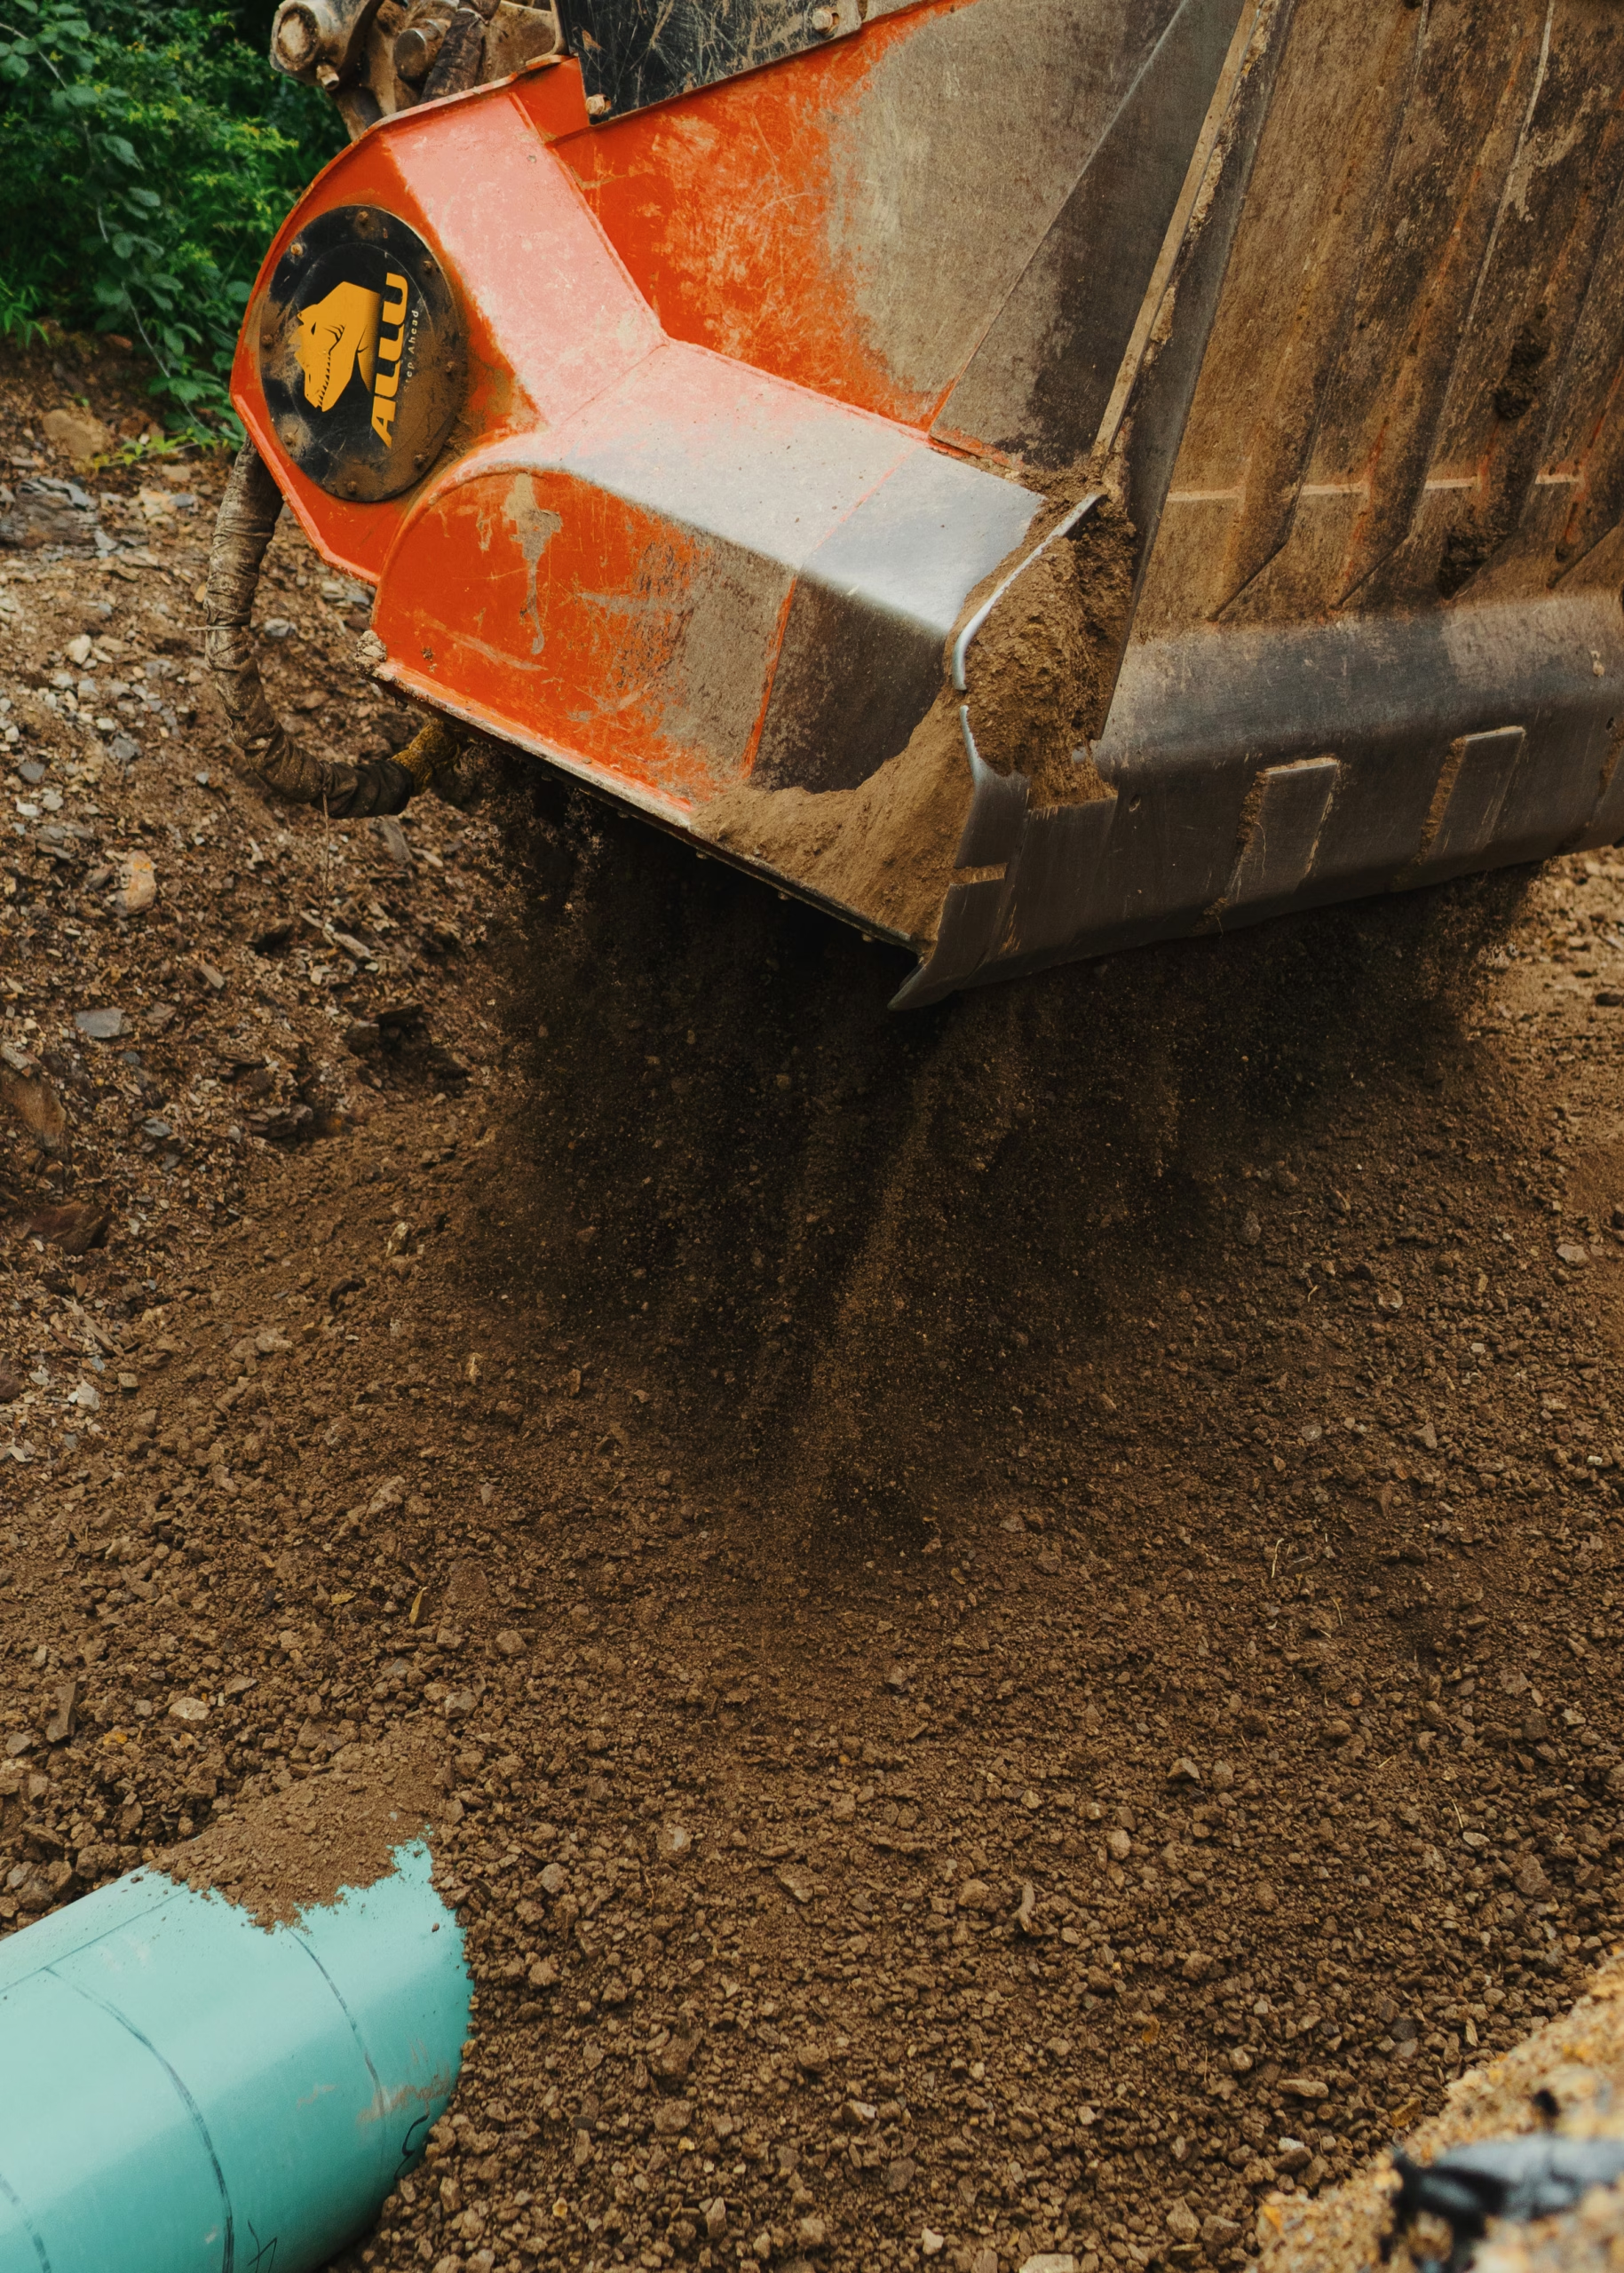
The ALLU padding bucket screening 1 ½” minus material from screened soil to protect the pipe coating.

For Momentum Pipeline Operations Manager Wade Mace, one of the biggest benefits of the ALLU bucket is how it has changed the company’s padding process. 

Before adopting padding buckets, the operation required a laborer to work in the ditch as an excavator gradually placed material. The laborer watched for larger rocks and manually removed them before they could come into contact with the pipeline. 

“The padding bucket has helped our productivity, it has taken labor out of [the project],” Mace said. “Now, with the padding bucket, that eliminates the labor in the ditch and has probably sped up the process by at least 2x.” 

By screening the material mechanically, Momentum Pipeline can reduce manual material sorting in the trench while keeping the padding operation moving. 

A 12-Year Relationship with ALLU

The West Virginia project is part of a much longer relationship between Momentum Pipeline, Leslie Equipment Company, and ALLU. 

“We’ve worked with ALLU buckets for 12 years now,” Mace said. “Our local dealer, Leslie Equipment, is a dealer of ALLU and that’s how we got hooked up with them.”  

Momentum Pipeline now has several ALLU buckets, and Mace said ALLU has remained the company’s choice for this type of work. 

“ALLU has been the only padding bucket we’ve used since we’ve been in business.” 

According to Mace, Leslie Equipment originally introduced the contractor to ALLU as pipeline padding practices evolved. The relationship has continued through equipment support and parts availability. 

“Leslie’s service with ALLU is great, no complaints at all,” Mace said. 

Dealer Support That Keeps Pipeline Projects Moving
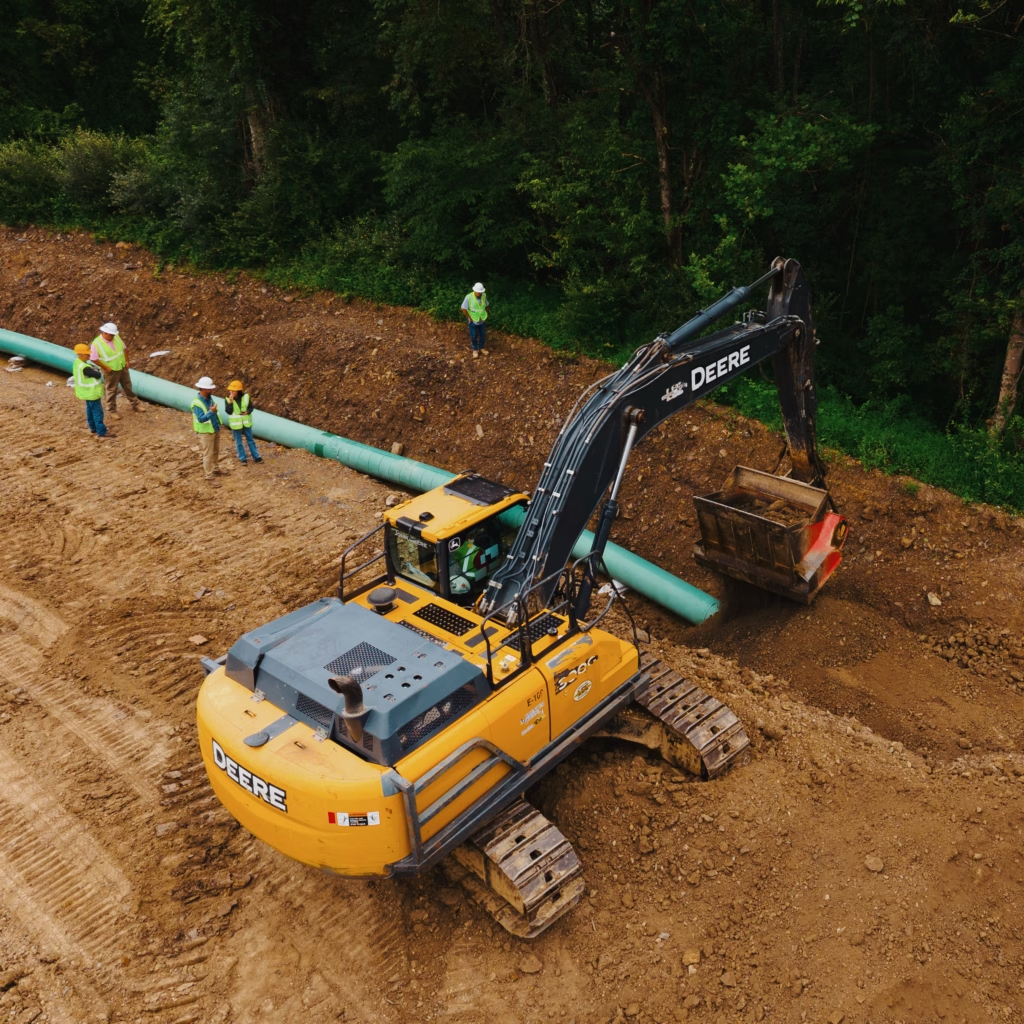
ALLU screening bucket mounted on a John Deere 300g excavator padding a pipeline in West Virginia.
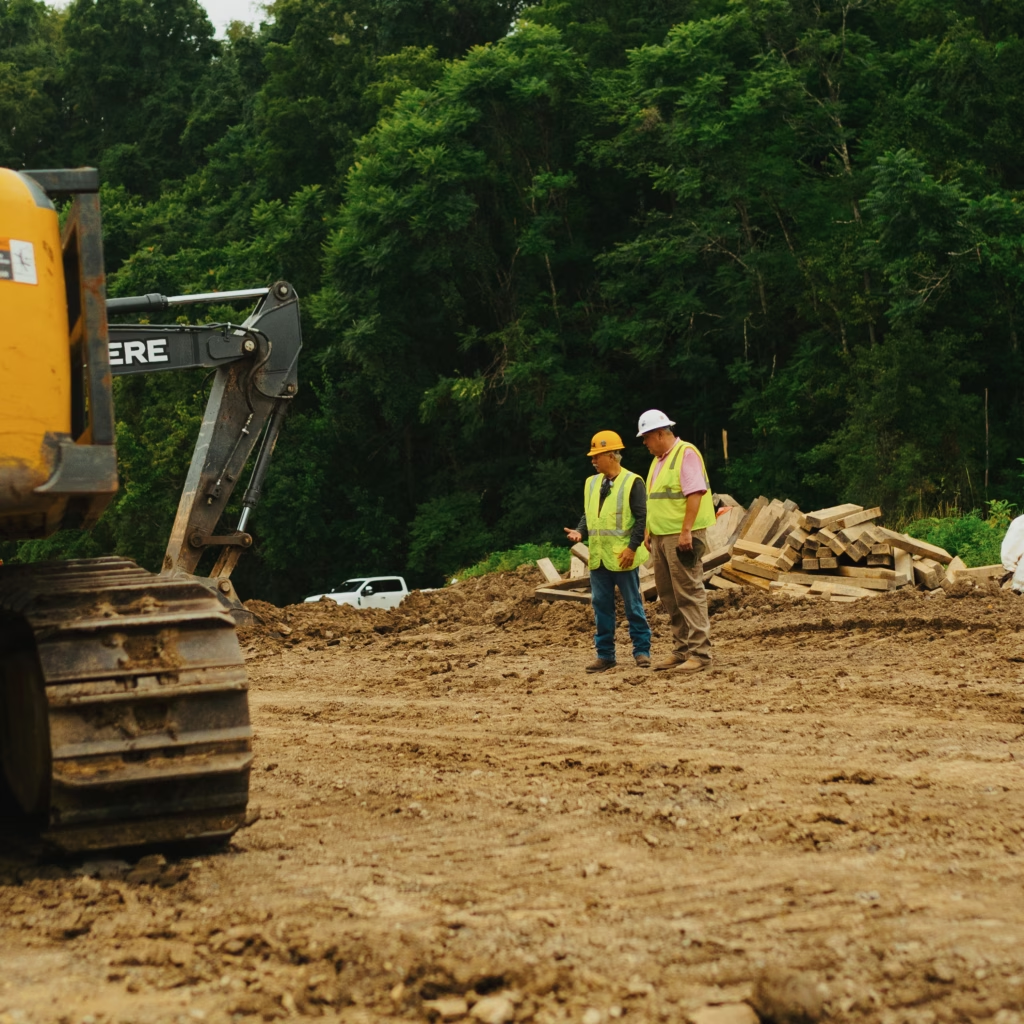
Two people discussing the work being done on the Pipeline project.

For Culicerto, productivity is only one reason Leslie Equipment continues to work with ALLU. Parts availability, equipment durability, dealer support, and the range of bucket sizes are also important when helping pipeline contractors select equipment. 

ALLU buckets can be matched to different carrier and project requirements, giving Leslie Equipment options for jobs ranging from smaller applications to commercial pipeline projects. 

“I would definitely recommend these buckets to anybody who needs pipelining, screening, crushing,” Culicerto said. “These are highly productive units with little to no downtime. Parts availability is great, and our dealer support is second to none.” 

Culicerto has also seen other bucket designs working in pipeline applications and points to ALLU’s productivity, including when conditions become wetter, as a reason Leslie Equipment prefers the ALLU equipment. 

For contractors, that combination of equipment and local dealer support can be particularly important on pipeline projects where keeping production moving is critical. 

A Proven Pipeline Padding Solution

For Momentum Pipeline, the West Virginia project demonstrates a process the company has relied on for years: combine ALLU screening technology with the equipment already working along the pipeline to efficiently produce padding material where it is needed. 

With Leslie Equipment Company and Pete Culicerto providing local equipment knowledge, bucket selection, parts availability, and support, Momentum Pipeline has access to both the attachment and dealer resources needed to keep its padding operation moving. 

After approximately 12 years of working with ALLU, Mace continues to recommend the equipment to other contractors. 

“We highly recommend ALLU to any other contractor or any other business,” Mace said. “They’re durable, the parts availability is great, and no complaints at all.” 

Watch the video to see the ALLU D-Series Buckets in action.

Screening Bucket – D-Series

Carriers 6 – 45 t
Versatile DN-, DS-, and DH-Series Screening Buckets serve in a wide range of applications, ensuring high-quality material processing on-site.

Other case studies

We solve problems

ALLU DH 3-17 working on an oil and gas pipeline backfilling job.

Turning Excavated Material into Quality Pipeline Backfill

On a 5-mile oil and gas pipeline project in Ohio, ALLU Screening Buckets transformed excavated soil into specification-ready backfill directly on-site. By screening and placing material with the same excavator,…

Explore customer story
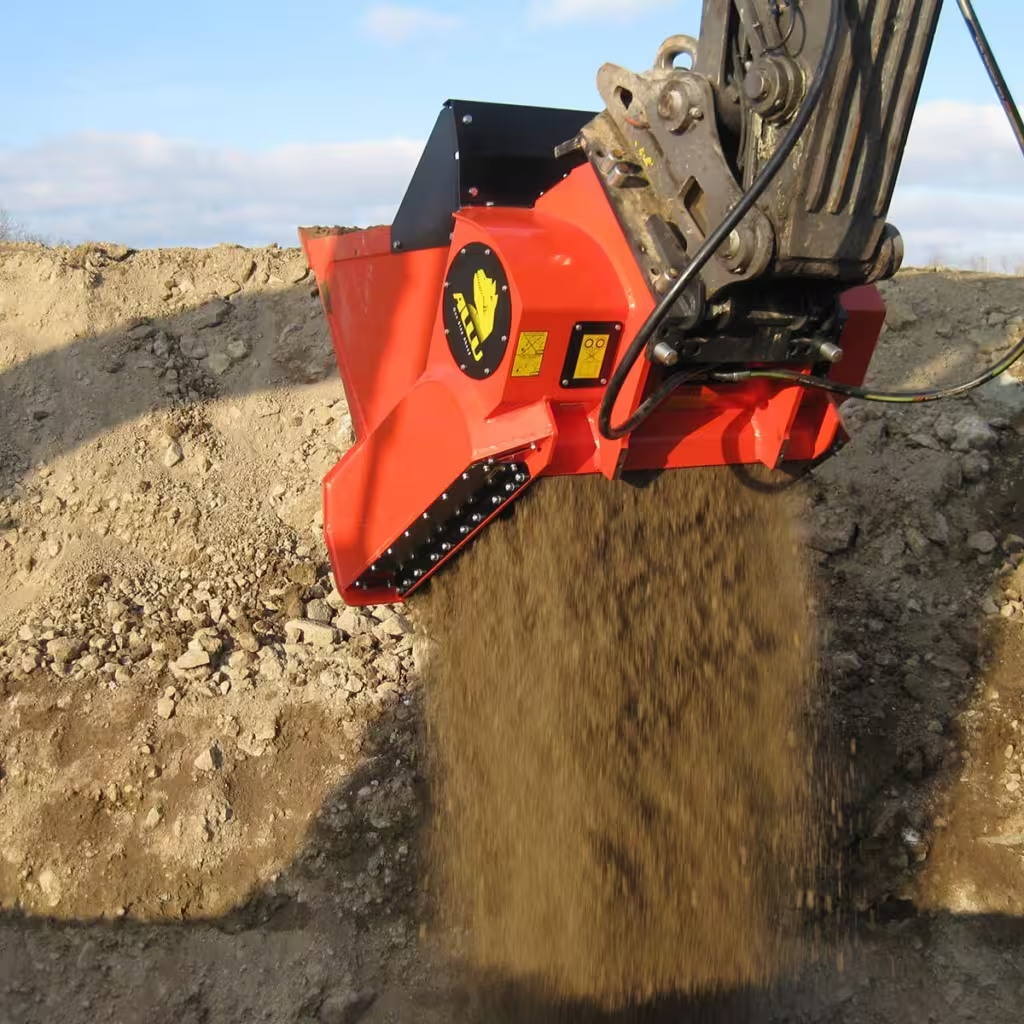
ALLU Transformer Screener Crusher Backfilling Pipeline

By re-using the material on site, there were no need to buy virgin material. ALLU Transformer screener bucket made the job efficient and saved on natural resources.

Explore customer story
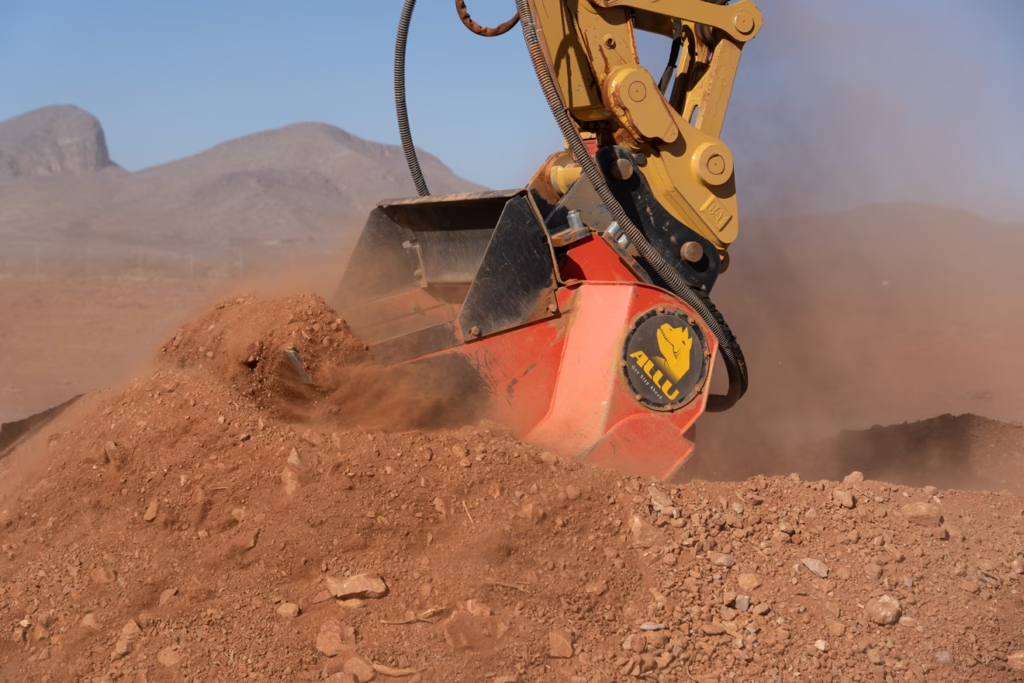
Better backfill in solar padding

To handle smaller jobs where large padding equipment didn’t fit, Ozzies brought in ALLU DN 3-12 buckets – screening material directly into trenches for solar, civil, and water projects with…

Explore customer story
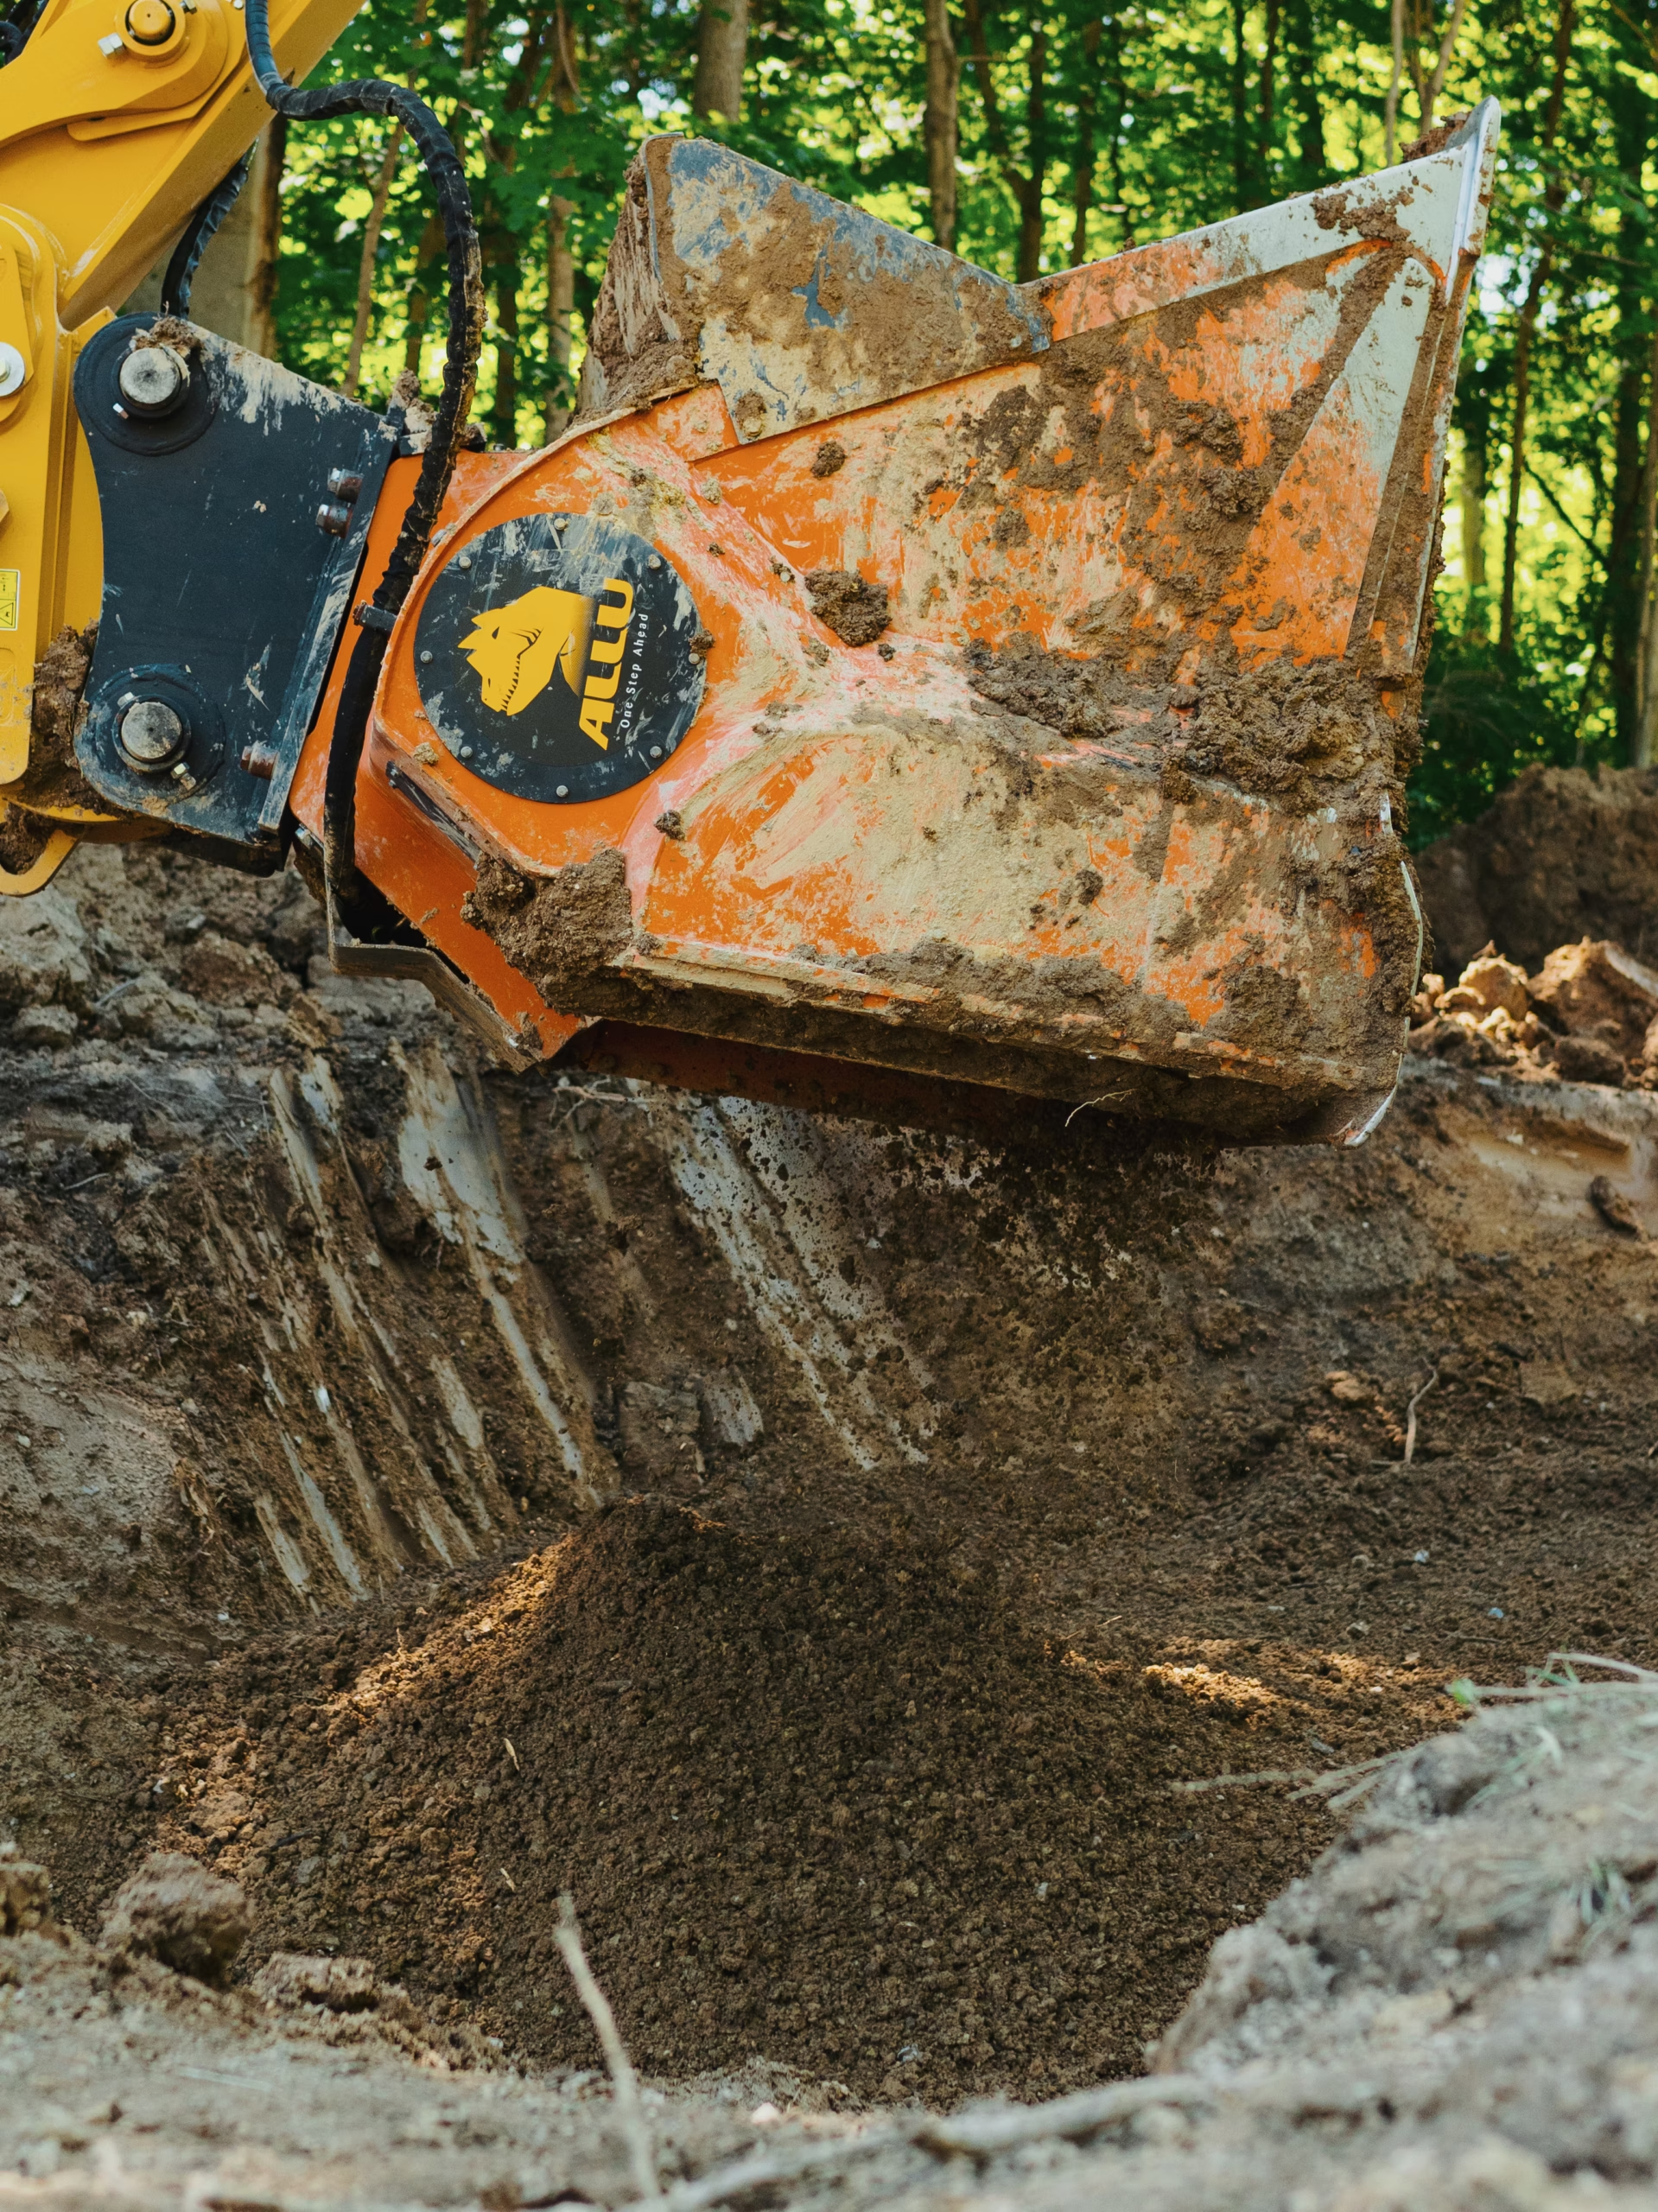
Rethinking Pipeline Backfill

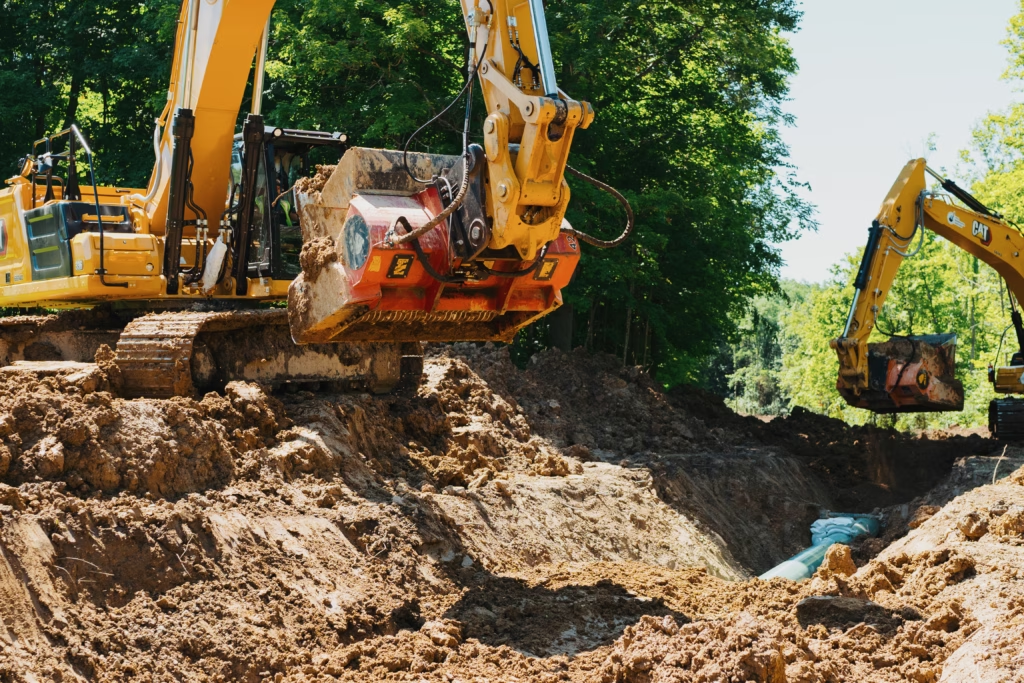
On this Dayton, Ohio pipeline project, an ALLU screening bucket helps process excavated material directly on-site, preparing it for backfilling while keeping the operation moving efficiently.
Case study

Turning Excavated Material into Quality Pipeline Backfill

Ohio, USA

Material 1” minus Material from Screened Soil

Industry Pipeline Padding

Application Pipeline & Utility Backfill

Function Padding Screened Material to Backfill and Protect Pipeline Project

Model ALLU DH 3-17 & DH 4-17 with 25mm XHD Drums

Pipeline backfilling is one of the most important stages of pipeline construction, providing a protective layer that helps safeguard the pipeline from damage while ensuring long-term stability and performance. Producing properly sized backfill material is essential to meeting project specifications, protecting pipeline coatings, and minimizing the risk of future maintenance issues. 

For many contractors, processing suitable material directly from the excavation can also reduce hauling, lower material costs, and improve overall jobsite efficiency. On a 5-mile oil and gas pipeline project in Ohio, these priorities led the contractor to partner with Leslie Equipment Company and utilize the ALLU DH 3-17 and DH 4-17 Screening Buckets to produce specification-ready backfill on-site, keeping material moving efficiently while supporting a streamlined construction process. 

The Importance of Backfill on an Oil and Gas Pipeline 

Proper backfilling and padding are essential to the long-term performance and safety of oil and gas pipelines. A layer of screened, fine material placed around the pipe helps protect the external coating from damage caused by rocks, debris, and other sharp materials during installation and throughout the pipeline’s service life. This protective cushion also provides uniform support, reducing point loading and minimizing the risk of settlement, movement, or stress on the pipeline as the surrounding soil compacts over time.  

By producing specification-compliant padding material directly on-site, contractors can improve construction efficiency, reduce the need for imported aggregates, and help ensure the pipeline is installed to the required project standards.  

With such a crucial job and high standards, it is important to use machines and attachments that will get the job done right the first time. Richard (Rick) Petty, who works in Leslie Equipment’s National Equipment Rentals Sales says, “I have worked with ALLU buckets since 2009, and ALLU has outperformed the competitor buckets every time.”  

Where ALLU Steps In 

The ALLU DH 3-17 and DH 4-17 Screening Buckets equipped with XHD 25 mm configuration are well suited for pipeline backfilling because they produce consistent, specification-ready material directly from excavated soil. By screening out oversized rocks and debris on-site, the buckets create a fine backfill material that helps protect pipeline coatings while providing uniform support around the pipe. On the Ohio jobsite, even in conditions of wet material and clay, ALLU still performed the job to meet quality expectations. 

Mounted directly to an excavator, the ALLU buckets allow contractors to screen and place material with the same machine, reducing equipment requirements and eliminating the need to transport excavated material to a separate screening plant. This efficient workflow helps keep pipeline construction moving while reducing hauling costs, fuel consumption, and dependence on imported backfill material. 

Safety and Cost-Savings in Mind 

Unlike traditional screening plants that require multiple machines, ALLU Screening Buckets screen and place padding material using the excavator already on the job. This efficient workflow helps keep pipeline projects moving while lowering operating costs and maximizing the value of existing material. Rick Petty shared, “With the ALLU padding buckets, you can get through the material pretty quick and get the pipe covered up and move on to the next part of the job.” 

Fewer support machines, truck movements, and material transfers help reduce congestion around the work area, creating a safer and more efficient jobsite for operators and ground crews. The bucket range also allows for smaller attachment usage, reducing weight on the machine and potential tipping.  

ALLU Screening Buckets are engineered to improve both safety and serviceability. Their durable, easy-to-maintain design allows routine service to be completed efficiently, helping minimize downtime while keeping operators and maintenance personnel safer throughout the project. 

Rick agrees, saying, “The serviceability of the ALLU buckets out here on a job really helps the customer with less downtime and more time padding pipe. These buckets are very efficient and can help the customer get their job completed quickly.” 

Watch the video to see the ALLU D-Series Buckets in action.

Screening Bucket – D-Series

Carriers 6 – 45 t
Versatile DN-, DS-, and DH-Series Screening Buckets serve in a wide range of applications, ensuring high-quality material processing on-site.

Other case studies

We solve problems

Hazardous Waste Processing in Latvia’s Largest Remediation Project

When Latvia launched its most ambitious environmental cleanup to date, A/S BAO turned to ALLU to handle the extreme materials and conditions at the infamous Inčukalns tar ponds. More than…

Explore customer story
Support by the bucketload: Enviropacific & ALLU

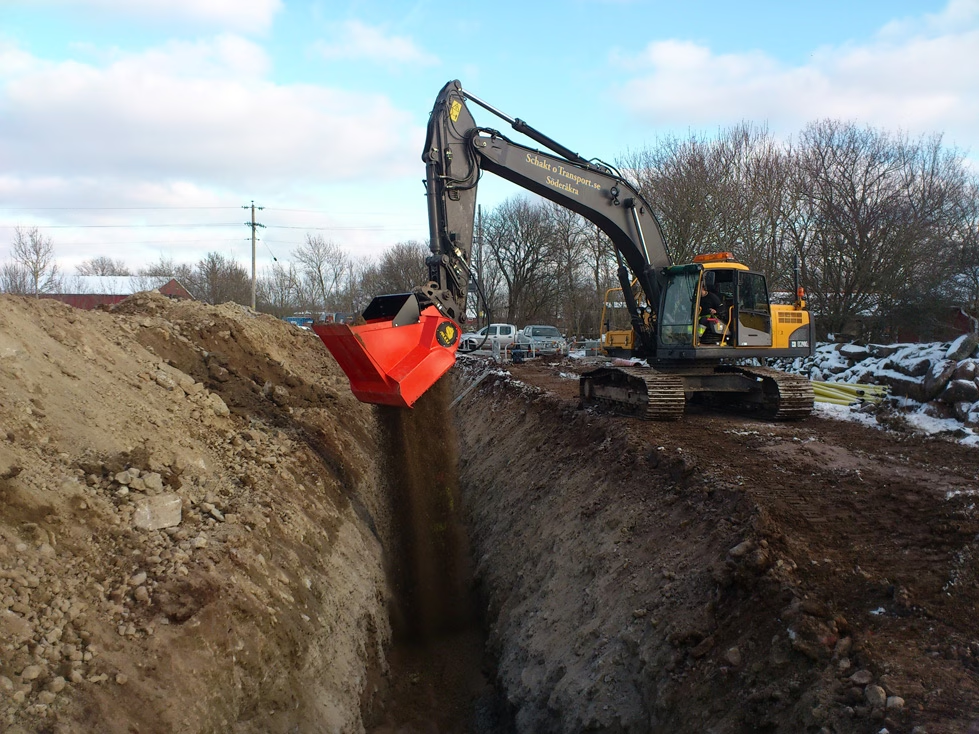
Enviropacific integrated a customised ALLU TS Screener Crusher bucket into their operations to address production challenges caused by tough clay material. The bucket, configured with axe blade cutters, was designed…

Explore customer story
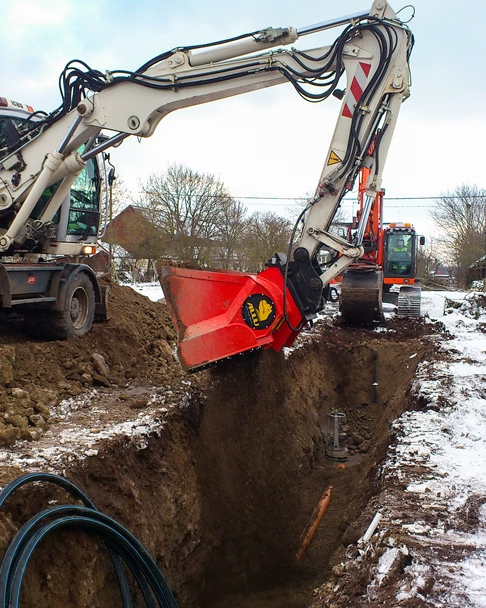
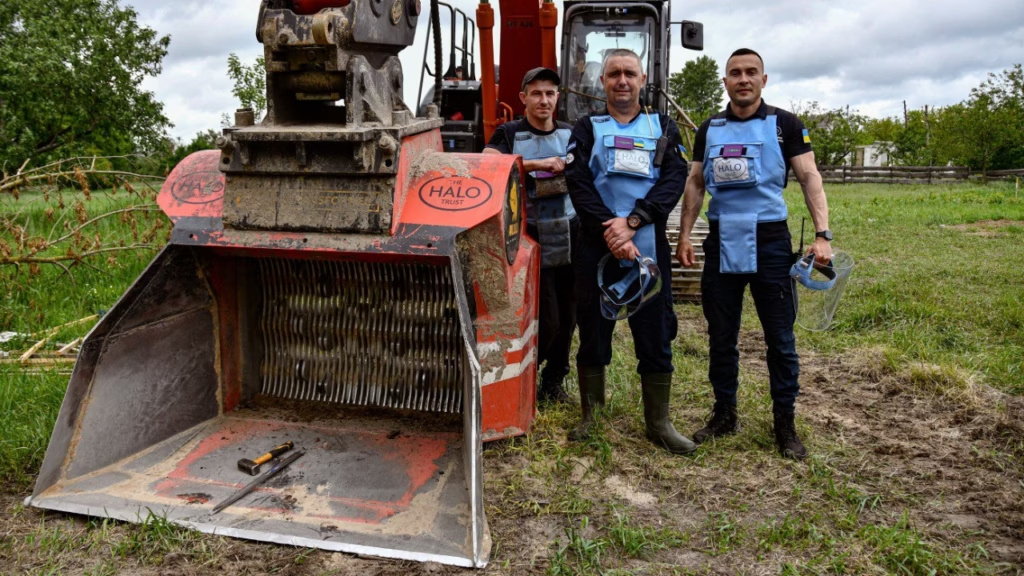
The HALO Trust uses ALLU screening buckets to improve mechanized demining operations in Ukraine.

ALLU screening buckets in demining

The HALO Trust is one of the world’s largest humanitarian demining organizations, working to protect lives and restore livelihoods in communities affected by conflict. In Ukraine, HALO uses ALLU screening…

Explore customer story
Solar Padding

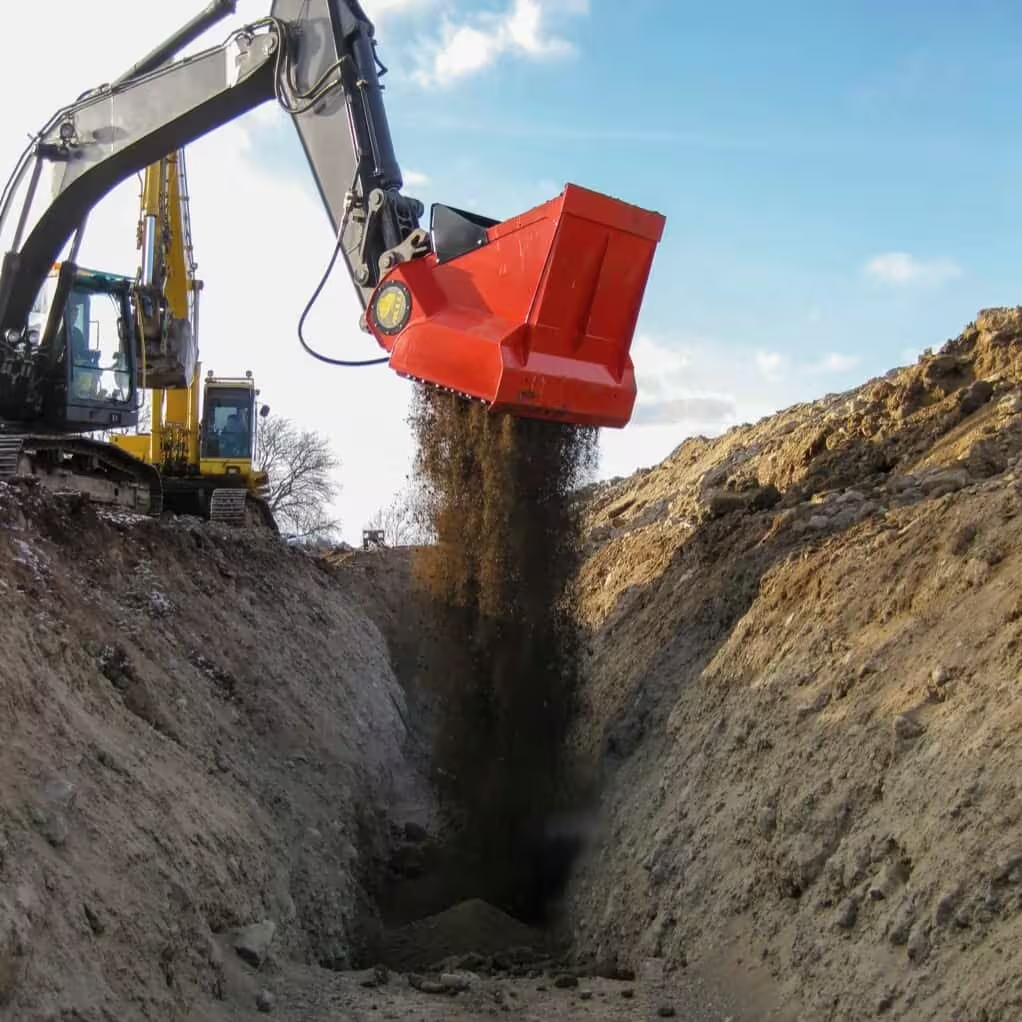
Ozzies combines ALLU buckets with their own machinery to deliver pinpoint backfilling for solar and civil projects across Arizona.
Case study

Better backfill in solar padding

Arizona, USA

Material 3/8″ minus material from screened soil

Industry Pipeline Padding

Application Pipeline & utility backfill, solar trenching

Function Accurate padding and screening for small project backfills

Model ALLU DN 3-12 with TS08 blades

Effective backfill separation can hugely improve project quality, save costs and improve sustainability. Pioneers of this mechanical process, with the development of their ‘Padder’ machine in 1989, Ozzies specialised machinery is now used far beyond their headquarters in Phoenix, Arizona, including in Europe, South America, Australasia and the Middle East.

Yet, despite this success, the business still strives to deliver more for its customers. So when their own machinery couldn’t cover all the tasks on smaller projects, they turned to the Screening and Crushing Buckets manufacturer ALLU. As Head of Sales and Rentals at Ozzies, Travis Casper explains. “We wanted to expand our equipment offerings at Ozzies to help our customers with more solutions. ALLU’s quality products were the answer we were looking for.”

Complete accuracy on small projects

“Some of the smaller jobs didn’t make sense for our own backfill equipment,” Travis admits. “Padding buckets like ALLU’s have a great place in our market. They can place material more accurately, which is important in certain projects.” These include renewable energy, pipeline construction and maintenance, civil construction and water projects, all of which Ozzies uses ALLU machinery for.

To deliver a greener, more efficient operation on a customer site in Phoenix, Arizona, the Ozzies team combined their machinery with two ALLU products, including the DN 3-12 TS screening bucket. Fitted with 8 mm solar blades (16 mm, 25 mm, 35 mm blade thicknesses are also available), the team can separate and place 3/8″ minus material accurately and efficiently.

Travis says, “The ALLU buckets can produce this material all day long and within spec. Then it can easily place material directly into the trench. The efficiency and exact placement of material from the ALLU Transformer series buckets is unmatched.”

Maximum ease and efficiency

By combining material screening and processing capabilities in one machine, the ALLU Transformer D-Series Buckets help teams work more efficiently without having separate equipment on site. Alongside pipeline backfills, the buckets are suitable for material handling jobs such as compost aeration, landscaping and construction waste treatment.

A hydraulic attachment that can be fitted to excavators and loaders with a plug-and-play installation, the buckets screen, crush, aerate, mix, separate, feed and load materials in a one-step operation.

Plus, as Travis explains, “Once the buckets and machines are set up with the proper delays, pressures and flows, it’s a pretty maintenance-free operation.”

The self-cleaning design minimises the likelihood of clogging and maximises capacity even with wet materials. With changeable blades and drums, the buckets can also be quickly adjusted for different tasks.

ALLU’s Variable Drum has a D-Series compatible frame and multiple ready-to-use drum sets. With individual shaft removal and a quick-locking two-bolt drum attachment system, different blade and drum types can be fitted or replaced without accessing the drive compartment. This makes maintenance and switching between screening and crushing tasks much more efficient, minimising downtime.

Similarly, ALLU’s Top Screen Rapid (TSR) blades make drum maintenance straightforward. Rather than opening the chain box and removing drums to change worn Top Screen (TS) blades, the two-piece structure of TSR blades means you can directly replace them on the shaft. Again, this cuts down on downtime significantly, reducing maintenance time by around two hours compared to standard blades.

With this mobile processing plant ready to take on customer sites, the team can deliver a project more efficiently, with a quality finish, while promoting sustainability and keeping costs low. With the ability to reuse leftover materials, less virgin product has to be purchased, transported to the jobsite or sent to a landfill. This cuts down on input costs, reduces fuel consumption and means waste materials are being recycled, which is great for Ozzie’s customers.

Boosting projects with a strong partnership

By connecting with ALLU, Ozzies have been able to take on more projects and better suit the needs of their customers. As Travis explains, “ALLU’s been a great partner for Ozzies and all our customers. They moved their headquarters to Nashville, Tennessee, which has been very helpful for us. To be centrally located and to deliver parts quickly and efficiently at a competitive price.”

Similarly, ALLU has been thrilled to see how Ozzie’s customers have benefited from using their products. As Jacqueline Day, Vice President of Marketing (North America) for ALLU, explains, “We are delighted to be working together in partnership with Ozzies, and they demonstrate an excellent use of the diversity and capability of the ALLU Buckets.”

Watch the video from Ozzies solar padding site.

Screening Bucket – D-Series

Carriers 6 – 45 t
Versatile DN-, DS-, and DH-Series Screening Buckets serve in a wide range of applications, ensuring high-quality material processing on-site.

Other case studies

We solve problems

Recycling of Asphalt, PFA, and More: ALLU & MRD Plant

Discover how MRD Plant in Leicestershire uses ALLU screening buckets, including the DH 4-17 and DS 3-23 models, to revolutionize waste material handling. From recycling asphalt road planings to processing…

Explore customer story

Hazardous Waste Processing in Latvia’s Largest Remediation Project

When Latvia launched its most ambitious environmental cleanup to date, A/S BAO turned to ALLU to handle the extreme materials and conditions at the infamous Inčukalns tar ponds. More than…

Explore customer story
Quarry waste screening with the ALLU bucket

Efficient Quarry Waste Handling

ALLU DH3-23 TS35 transforms quarry waste into valuable resources. By efficiently separating stone and clay, larger stones are ready for resale, and fine materials are repurposed for road construction or…

Explore customer story
ALLU DS 3-23 Transforms Recycled Asphalt at Finland's Largest Asphalt Plant | Asfalttikallio

Asphalt Recycling: Finland’s Largest Plant

Finland’s largest asphalt contractor, Asfalttikallio, uses ALLU DS 3-23 to transform cold milled asphalt into quality material for production. Operating at their advanced Ylöjärvi facility, they process recycled asphalt efficiently…

Explore customer story
conversion of recycled soil into beneficial products like manure and garden mixes

Soil Recycling Management in Australia

Soil Recycling Co. is at the forefront of soil screening in Victoria, dedicated to promoting the reuse of soil as a valuable resource rather than disposing of it in landfills.

Explore customer story

Pipeline padding in Sweden

See how NCC optimized pipeline padding in Öland with ALLU screening buckets, transforming on-site material handling while reducing costs and environmental impact.
Case study

Pipeline padding in Sweden

Öland, Sweden

Material Excavated soil for backfilling

Industry Pipeline Padding

Application Pipeline padding and backfilling

Function Screening and reusing excavated material for pipeline backfill

Model ALLU DS4-12 and DN3-12 screening buckets

Transforming Pipeline Projects in Sweden’s Island Community

In a residential area on Öland, Sweden, a pipeline renewal project demonstrated how modern approaches to material handling can reshape traditional construction methods. NCC, working with their subcontractor Schakt & Transport, tackled a water pipeline upgrade that would typically involve significant material transport logistics and associated costs.

a pipeline renewal project demonstrated how modern approaches to material handling can reshape traditional construction methods.

Rethinking Pipeline Construction

NCC, one of the leading construction and infrastructure companies in Northern Europe, partnered with local contractor Schakt & Transport for this residential pipeline project. With operations across Sweden, Norway, Denmark, and Finland, NCC brings extensive experience in infrastructure development. Their commitment to sustainable construction practices made them particularly receptive to innovative solutions for this Öland project.

In conventional pipeline projects, contractors often face a significant challenge: excavated material needs to be transported away while new backfill material must be brought in. This creates a complex logistical operation involving multiple trucks, increased traffic in residential areas, and substantial material costs. Drawing on their extensive experience in infrastructure projects, NCC’s team recognized an opportunity to approach this differently.

pipeline padding project in Sweden

A Tailored Two-Bucket Solution

The project utilized two ALLU screening buckets, each serving a specific purpose in the operation. The larger DS4-12 bucket handled the main pipeline trenches, processing larger volumes of material efficiently. For the more intricate work around service connections and narrower trenches, the DN3-12 provided the precision and maneuverability needed. This dual-bucket approach ensured that every aspect of the project could be handled with maximum efficiency.

From Challenge to Opportunity

Instead of treating excavated soil as waste that needed to be removed, the team repurposed it into a valuable resource. The ALLU screening buckets processed this material on-site, creating backfill that met all technical specifications. This approach eliminated the need for purchasing and transporting new aggregate, while ensuring that the backfill material maintained consistent quality throughout the project.

Beyond Cost Savings

While the immediate financial benefits were significant, the project’s impact extended far beyond the budget. The residential community benefited from reduced construction traffic, as fewer trucks needed to access the site. The environmental footprint of the project was substantially reduced, both in terms of material usage and transport emissions. The streamlined operation also meant faster project completion times, minimizing disruption to local residents.

Setting New Standards

The success of the Öland project demonstrates how innovative approaches to material handling can transform pipeline construction. By choosing the right equipment and rethinking traditional methods, contractors can achieve better results while reducing costs and environmental impact. The combination of ALLU’s versatile screening technology and thoughtful project planning proved that sustainable practices and operational efficiency can go hand in hand.

Key Project Benefits:

  • Significant reduction in material and transport costs
  • Minimal environmental impact through material reuse
  • Enhanced project efficiency with optimized equipment selection

Looking Ahead

For contractors in pipeline construction, ALLU Transformer screening buckets provide a smarter, more cost-effective way to handle material on-site. Instead of hauling excavated soil away and paying for new backfill, they allow teams to process and reuse existing material directly in the trench, cutting costs and streamlining operations.

With the ALLU DS4-12 and DN3-12, NCC and Schakt & Transport completed the project without the need for external material deliveries, reducing truck traffic, fuel consumption, and overall project expenses. A practical solution that keeps the job moving efficiently while making the most of available resources.

Screening Bucket – D-Series

Carriers 6 – 45 t
Versatile DN-, DS-, and DH-Series Screening Buckets serve in a wide range of applications, ensuring high-quality material processing on-site.

Other case studies

We solve problems

Pipeline Padding in France

Excavated material unrefined cannot be used to backfill for pipeline padding. The customers costs were increasing to remove the material and bring in correct material to site.

Explore customer story

ALLU Transformer Screener Crusher Backfilling Pipeline

By re-using the material on site, there were no need to buy virgin material. ALLU Transformer screener bucket made the job efficient and saved on natural resources.

Explore customer story
Case study

Pipeline Padding in France

France

Material Pipeline padding

Industry Pipeline Padding

Application Pipeline padding

Function Pipeline

Model ALLU D-Series

Problem

Excavated material unrefined cannot be used to backfill for pipeline padding. The customers costs were increasing to remove the material and bring in correct material to site.

Solution

The ALLU D-Series of screening buckets with TS drums for pipeline padding is an absolutely ideal addition to pipeline job sites worldwide. The unique ALLU TS structure enables two different fragment sizes from the same ALLU Screening Bucket, giving you more flexibility at the site. Due to TS’s self-cleaning design, you can be certain to get the best possible capacity even with wet and sticky materials. ALLU TS structure features various blade thicknesses, making the TS structure perfectly suited to the pipeline industry to screen, reuse, and recycle the excavated soil.

Benefit

The customer increased efficiency and reduced costs and time. As they do not need to bring in separate materials to the jobsite or take those materials away.

Related Products

Case study

ALLU Transformer Screener Crusher Backfilling Pipeline

Sweden

Material Soil

Industry Pipeline Padding, Screening

Application Pipeline padding

Function Pipeline padding, Screening

Model ALLU Transformer DSB 3-12 screener crusher with TS 25 blade setup

Problem

Pipeline required backfilling and refilling the pipeline with new material would have caused additional costs for the project.

Solution

 The excavated material from the pipe trench was screened back to the trench with the ALLU Transformer screener crusher and the original material was used as backfilling. The ALLU Transformer screener bucket was able to screen reusable material for pipeline backfilling, meaning no additional material costs.

Benefit

By re-using the material on site, there were no need to buy virgin material. ALLU Transformer screener bucket made the job efficient and saved on natural resources. The job site traffic was also minimized due to utilizing the existing material with only one machine.  

Related Products